THE CHALLENGE
A large consulting and contracting firm owns and operates several ex-situ Thermal Desorption Units (TDUs) approved for use under the Resource Conservation and Recovery Act (RCRA); the Comprehensive Environmental Response, Compensation and Liability Act (CERCLA); as well as for use at private industrial remediation sites containing a wide variety of chlorinated and non-chlorinated contaminants up to concentrations of 3,000 ppmv. Being mobile, the TDUs can be deployed anywhere in the country and would be subject to varying local environmental regulations on hydrogen chloride (HCl) emissions produced from the thermal oxidation of halogenated compounds. Lastly, the operating cost of the full remediation solution directly affects the total project cost and ultimately the firm’s bottom line. To meet their technical and commercial project requirements, the customer was seeking an Air Pollution Control solution capable of handling a wide range of contaminants and mitigating HCl emissions all while being easily mobilized and possessing the lowest operational cost possible.
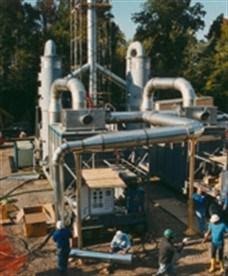
After a thorough technical evaluation and bid process, the customer selected a complete, mobile treatment package from Anguil Environmental Systems’ Wastewater Treatment team (FKA Global Technologies), containing a Chlorinated Catalytic Oxidizer (Chloro-Cat) and acid gas scrubber package. Anguil’s solution was selected due to our experience with over 30 such systems already installed to treat similar chlorinated streams from Soil Vapor Extraction sites as well as groundwater remediation sites utilizing air strippers.
THE SOLUTION
 A catalytic solution was selected largely due to the oxidizer’s compact body and ability to operate at lower combustion temperatures, making it mobile and cost effective to run as compared to a traditional Direct Fired Thermal Oxidizer. The lack of inexpensive natural gas feeds at many remediation sites dictates the use of propane for supplemental fuel and because direct thermal oxidation requires operating at temperatures between 1600°F – 2000°F considerable amounts of costly propane would be consumed over the course of the project. By contrast, each TDU could be expected to exhaust up to 5,000 SCFM of desorption air at temperatures between 400°F – 900°F which is at or near the minimum inlet catalyst temperature. Because the incoming process temp was already preheated by the TDU little supplemental fuel would be required by the Chloro-Cat. As with all Anguil chlorinated catalytic systems, a 316L stainless steel shell and tube heat exchanger would be installed in the 316L stainless steel reactor to further minimize propane consumption.
To mitigate HCl emissions, Anguil utilized a high temperature quench on the Choro-Cat exhaust followed by an acid gas scrubber constructed of Fiberglass Reinforced Plastic (FRP). HCl is removed from the air stream by interaction with either a recirculating caustic solution or using once through water. An induced draft FRP fan on the back end of the treatment package was provided to pull vapors through the system due to the high temperature, highly saturated exhaust from the TDU and the resultant HCl acid gasses.
As this was a soil heating application, utilization of a high-temperature baghouse dust collector on the TDU skid removed concerns associated with dust or dirt plugging of the monolithic catalyst cells.
Anguil was able to package the entire system onto a 50′ drop deck trailer. In addition to the Chloro-Cat and scrubber, the trailer included a Liquid Propane Vaporizer and a storage area for equipment transport.
THE RESULT
Anguil’s experience proved invaluable in designing and implementing the proper solution for this application. The chlorinated catalytic system was designed to provide 99% destruction efficiency at operating temperatures of 500°F – 850°F to reduce auxiliary fuel usage and meet the customers’ needs for performance and low OPEX. Safety systems were installed to ensure no HCl condensation to minimize equipment corrosion to protect the customer’s investment, and with the modular trailer mounted solution, eased the customer’s ability to deploy to multiple sites. The most recent compliance testing of this turnkey package demonstrated over 99% destruction of all compounds.