Ensure Production Uptime.

Anguil’s engineering expertise and flexible solutions guarantee compliance and optimized performance so your chemical plant can focus on production.

Applications

  • Process, Tank Vent & Fugitive Emissions
  • Amine Tail Gases
  • API Oil-Water Separator Discharge
  • Process Wastewater Treatment
  • Chemical Polymerization

Challenges Solved

Is this you?

  • Your process contains acids as well as halogenated and chlorinated compounds
  • Your emission streams can sometimes be inert, or lacking oxygen
  • Your wastewater discharge requirements have gotten more stringent
  • Reliable operation of your processes is a top priority

The Anguil Advantage

The Chemical Processing Industry (CPI) is a diverse sector of the world economy that supplies a variety of raw materials to related industries. Because of this, many chemical companies operate under demanding production schedules with challenging environmental requirements. Increasingly stringent clean air standards are forcing chemical processing companies to pay more attention to the design, operation and maintenance of air pollution control equipment.

Selecting the proper abatement system and supplier can mean the difference between regulatory compliance and a process shutdown.  Anguil Environmental has been supplying off-gas treatment systems to the chemical processing industry for decades.  Our vapor combustion and oxidation technologies have been successfully applied on numerous processes, from tank vents and API separators to mixing operations and coating applications.  We design, manufacture, install, and service thermal and catalytic oxidizers and vapor combustors that offer high destruction efficiency, low operating cost, system reliability and minimal carbon output.  In addition, we have the necessary experience to control halogenated streams containing chlorinated, brominated and fluorinated compounds which are often emitted during chemical processing.

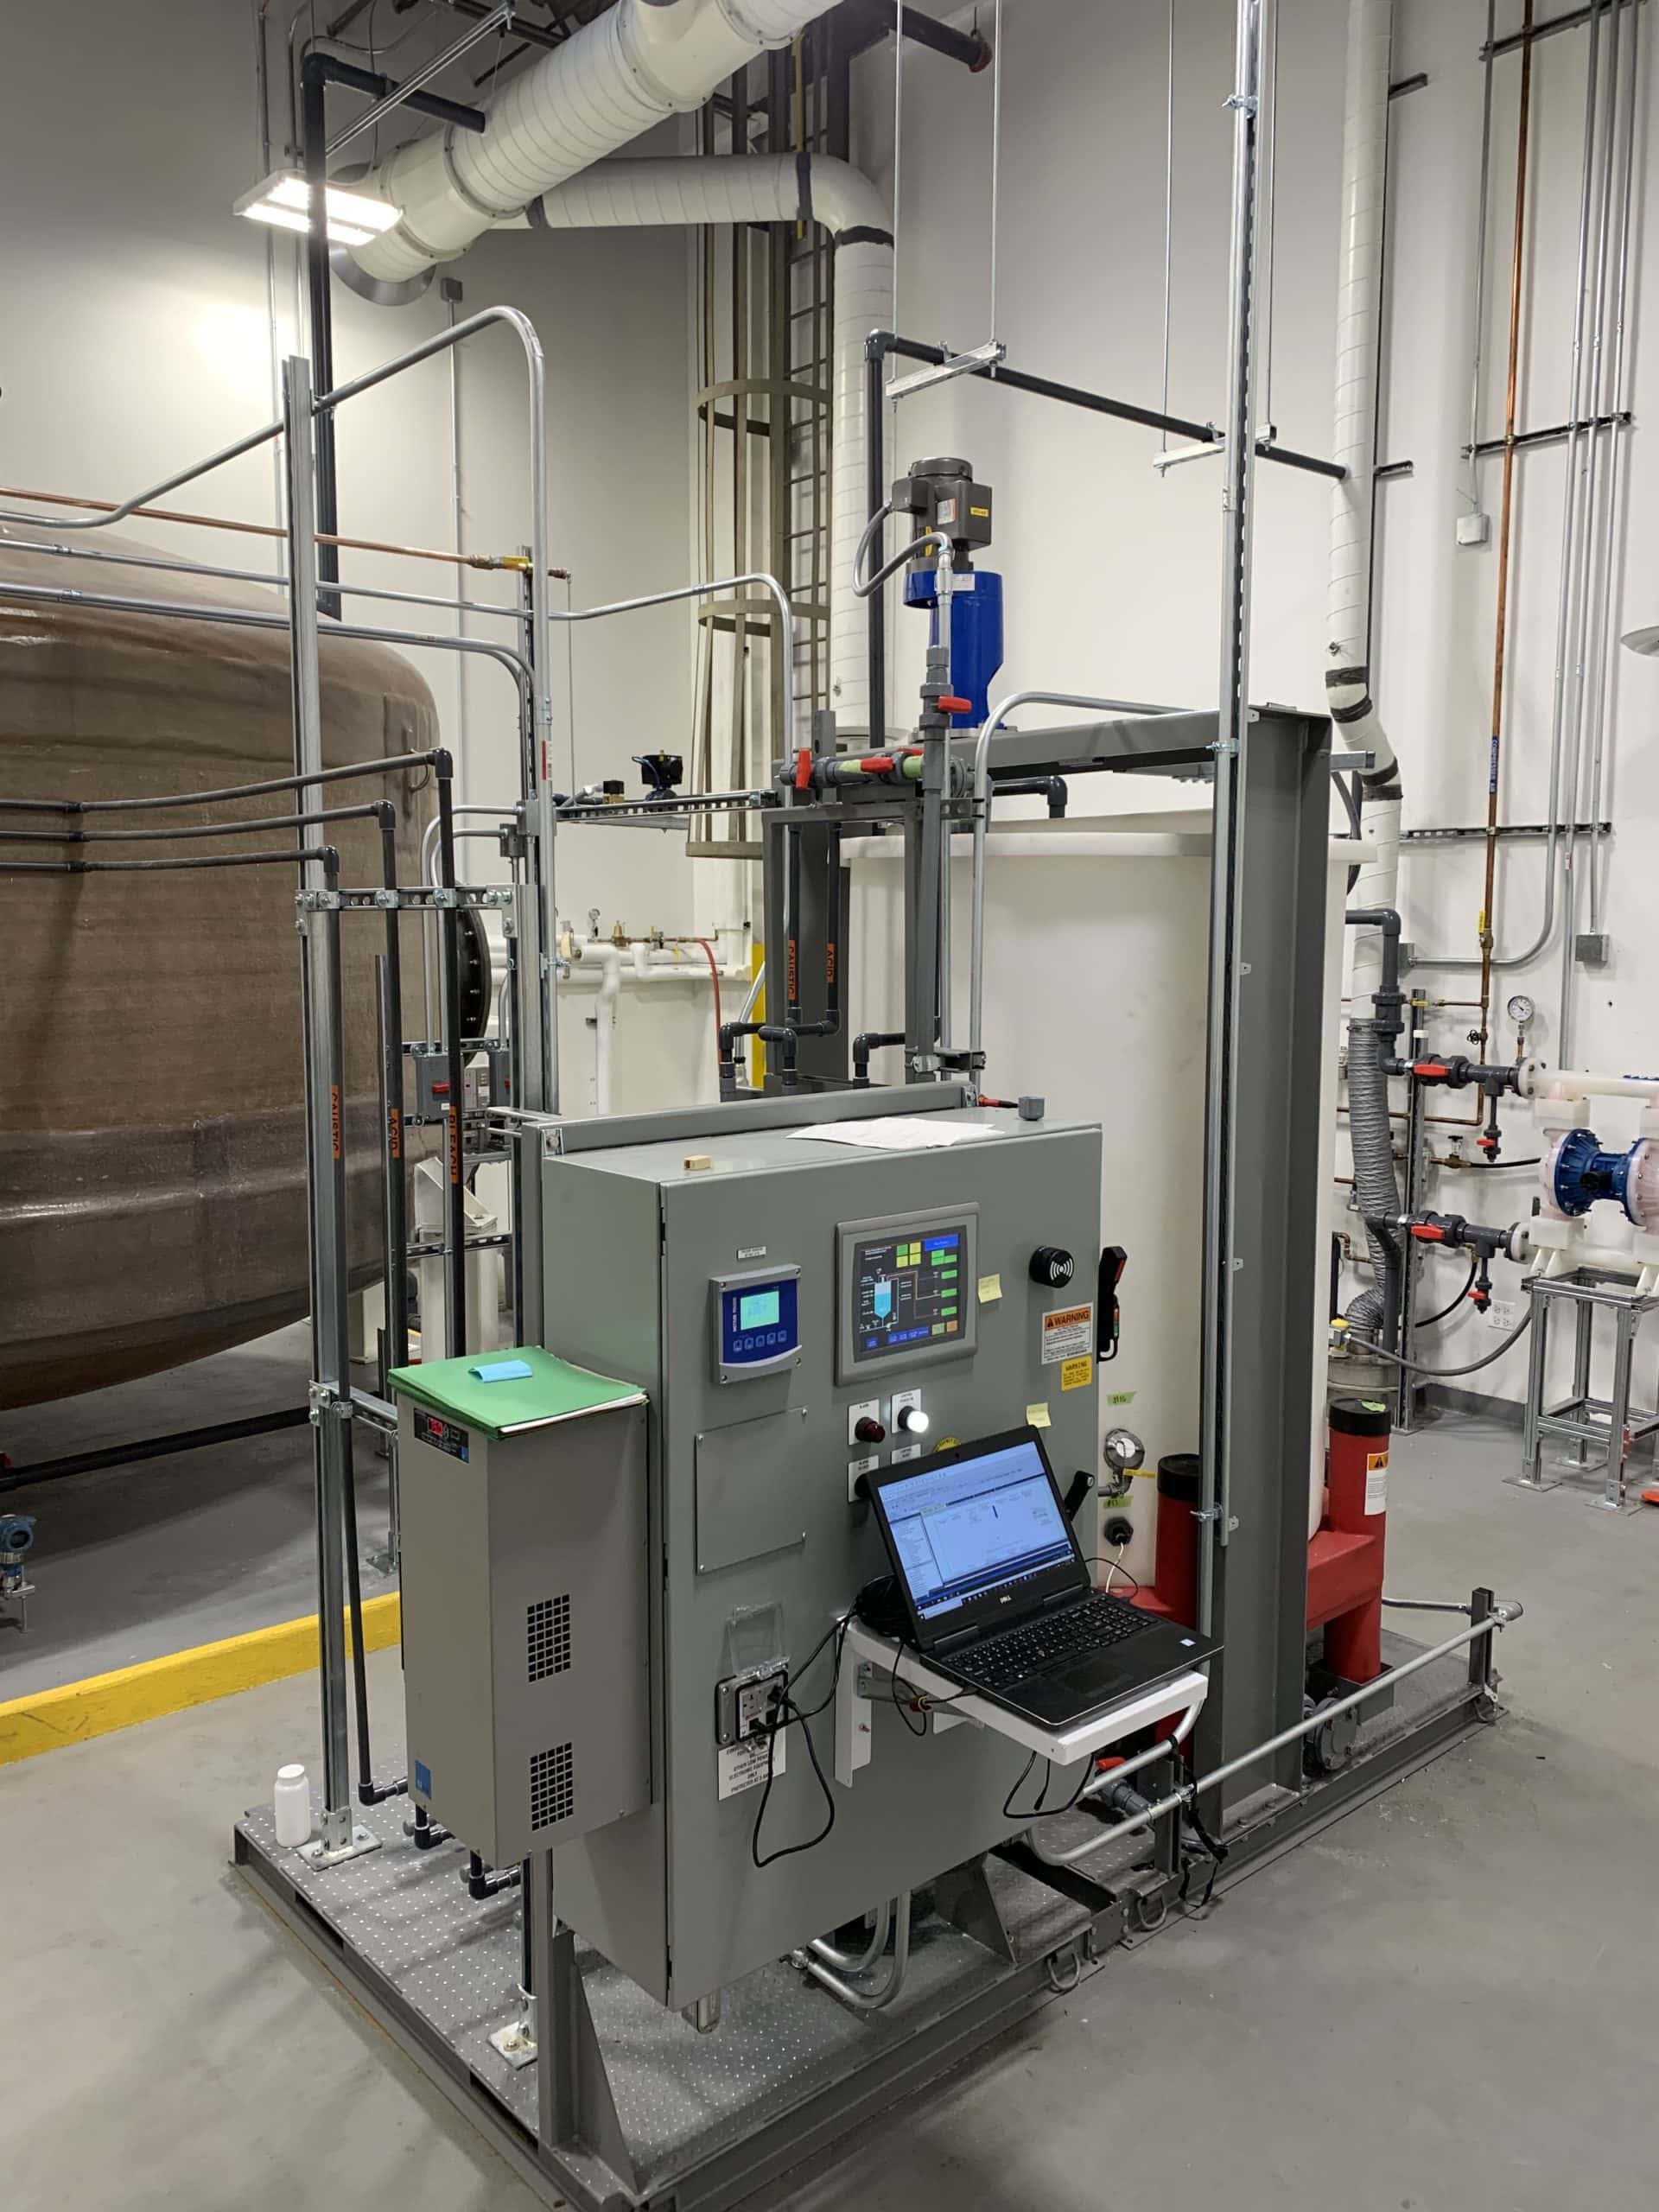
On the water side, Anguil provides turnkey water treatment systems that target solid or liquid pollutants from industrial and remediation applications.  As a custom solution company, we can integrate a range of technologies with proven techniques to meet specific site challenges at specialty chemical and petrochemical operations that process organic and inorganic raw materials.

System Solutions

We custom engineer each solution, but Anguil finds the following technologies to be especially effective for chemical industry applications:

  • Solutions In Action

Resources