


A Single Solution for Both VOC Gases and Waste Liquid for Propylene Production
Comments Off on A Single Solution for Both VOC Gases and Waste Liquid for Propylene ProductionTHE CHALLENGE

A leading petrochemical company in China constructed a new propylene oxide (PO) production facility. The process generates substantial volumes of waste gas and liquid containing a complex pollutant mix: VOCs including methanol, ethanol, propylene oxide and acetone, along with inorganic compounds such as nitrogen, ethane, propylene, propane, hydrogen peroxide, methyl ether, methane, and hydrogen.
As environmental regulations in China continue to tighten, local authorities required a dedicated treatment system meeting the national standard GB31571-2015 for petrochemical industry and applicable provincial standards before the plant could commence operation.
TAKING ACTION
To address this critical need, the petrochemical company turned to again Anguil. They had prior experience with Anguil equipment having two treatment systems installed for other applications in the region which demonstrated stable long-term performance. Based on this track record, the client commissioned Anguil to design, supply, and commission the treatment system for the new PO plant.
THE SOLUTION
After conducting a comprehensive analysis of the waste stream composition, emission requirements, and operational conditions, Anguil engineers designed a tailored solution for the unique process: an integrated system combining a Thermal Oxidizer (TO), waste heat boiler, Selective Catalytic Reduction (SCR) denitrification unit, economizer, and activated carbon adsorption backup system. This combination was chosen for its ability to address the complex pollutant mix, meet strict emission limits, and deliver economic and environmental benefits.
Waste Gas and Liquid Profile
The streams to be treated originate from multiple process points across the PO plant, including reactors, separation columns, and the intermediate tank farm. Composition, flow rate, and thermal content differ significantly across these sources. Several streams carry high concentrations of combustible organics with wide flammability ranges; others are inert-heavy or dilute. A portion of the pollutant load is in liquid phase, requiring atomized injection rather than standard gaseous feed. This variability demanded a purpose-designed inlet and combustion configuration to ensure complete treatment across all operating scenarios.
Process Flow: From Contamination to Compliant Emission Exhaust

- High-Temperature Oxidation: Combustible pollutants in the waste gas and liquid are injected into the TO via specialized nozzles, atomized with steam for optimal dispersion. Operating at a high temperature of 1,100 ℃, the TO oxidizes the contaminants in an oxygen-rich environment, converting them into water and carbon dioxide.
- Waste Heat Recovery: The high-temperature purified flue gas (carrying substantial thermal energy) is directed to a waste heat boiler that recovers the thermal to produce 30 t/h of superheated steam at 2.4 MPa. The client can reuse the steam in the PO plant’s production processes.
- Denitrification (SCR): High-temperature combustion in the TO produces thermal NOx as a byproduct. To bring NOx within regulatory limits, flue gas is cooled to approximately 320 ℃ and is routed to an SCR unit, where NOx is reduced to nitrogen and water through catalytic reactions, ensuring compliance with NOx emission standards.
- Secondary Heat Recovery: To maximize energy efficiency, an economizer (equipped with a deaerator) is installed at the SCR outlet. This device preheats boiler feedwater by using the remaining thermal from the flue gas, lowering the final exhaust temperature to 160 ℃, improving overall thermal efficiency and reducing stack heat losses.
- Final Emission: The treated flue gas is drawn through a negative-pressure fan and discharged into the atmosphere via a stack, fully meeting the required environmental standards.
Key Advantages of the Integrated System
The solution was designed to address not just compliance, but also the client’s operational and economic needs—offering five core advantages:
High Destruction Efficiency with Energy Saving
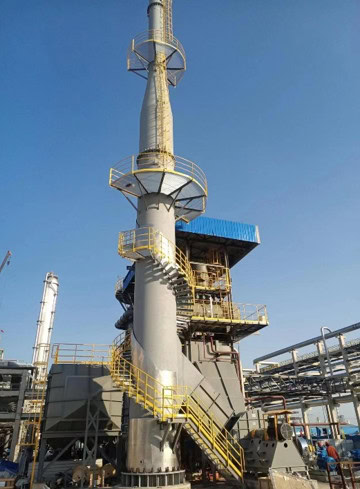 The TO is the heart of the system, delivering a pollutant destruction efficiency above 99.9% while optimizing energy use:
- Complete Oxidation: The TO’s design—including strategically selected and positioned burners, plus internal baffles—ensures thorough mixing of waste gas/liquid and combustion air. The baffles extend the flue gas residence time and promote turbulence, guaranteeing the complex pollutants are fully oxidized.
- Energy Recovery: The waste heat boiler transforms waste thermal energy into usable steam, creating significant economic value. The steam output is matched to the PO plant’s process requirements and fed directly into the plant’s utility distribution system, displacing equivalent natural gas-fired steam generation. At current energy prices, this represents over RMB 50 million in annual economic benefits for the client—turning a compliance cost into a revenue-generating asset.
Smart Burners: To adapt to the plant’s varying operational conditions, combined burners were utilized. This design reduces the total number of burners required and allows real-time adjustment of fuel output to match varying waste gas volumes, minimizing supplemental fuel consumption while maintaining stable combustion temperature.
Superior Safety Assurance
Safety is paramount in petrochemical operations, and the system was engineered to meet the highest global standards:
- Compliance with International Standards: The TO is designed in accordance with the U.S. NFPA 86 standard, a globally recognized benchmark for thermal oxidizer safety.
- Hazard Analysis & Simulation: A Hazard and Operability (HAZOP) analysis is conducted to identify and mitigate potential risks. Advanced simulation tools were also used during the design phase to optimize system parameters, ensuring safe operation under all expected conditions.
Explosion‑Proof and Safety Instrumentation Provisions: All field instruments are specified to explosion-proof standards. Flame arrestors, combustible gas detectors, and emergency shutoff valves are installed at critical inlet and outlet points.
Low Failure Rate for Reliable Long-Term Operation
To minimize downtime and maintenance costs, the reliability is prioritized in component selection and system design:
- High-Quality Components: Electrical and instrumentation parts are sourced from internationally recognized, industry-proven brands—ensuring durability and performance.
Optimized Controls: Rational control system design reduce the risk of component failure, ensuring the system operates stably with minimal interruptions.
Simple and Convenient Operation
The entire system is fully integrated with a Distributed Control System (DCS) and Safety Instrumented System (SIS), enabling full automation. No dedicated on-site operators are required for routine operation—only regular inspections are needed. Both systems allow remote monitoring and control, simplifying management and reducing labor costs.
Emergency Backup for Uninterrupted Compliance
An activated carbon adsorption system is dedicated to the intermediate tank farm’s waste gas. Under normal operation, this stream is processed through the TO. When the TO is offline for planned or unplanned maintenance, the tank farm exhaust is automatically diverted to the adsorption unit, where VOCs are captured before discharge via stack. This maintains continuous compliance without requiring additional operator intervention.
THE RESULTS
Since commissioning, the system has operated stably with no significant unplanned downtime. Destruction efficiency is maintained at 99.99%, and emissions of NMHC, acetone, phenols, methanol, and NOx consistently remain below the limits defined in GB31571-2015 and DB32/315-2016. The project met the environmental compliance requirements for the new production unit and has supported uninterrupted operation since startup.
The system’s consistent performance reinforced the client’s confidence, and they subsequently selected Anguil to design and supply waste gas treatment equipment for another new production facility. That project equally met all design requirements and performance targets upon commissioning. The repeat engagement reflects the client’s sustained satisfaction with Anguil’s technical capability and long-term service support.
From Bottleneck to Breakthrough: Transforming Wastewater into a Growth Enabler
Comments Off on From Bottleneck to Breakthrough: Transforming Wastewater into a Growth EnablerTHE CHALLENGE
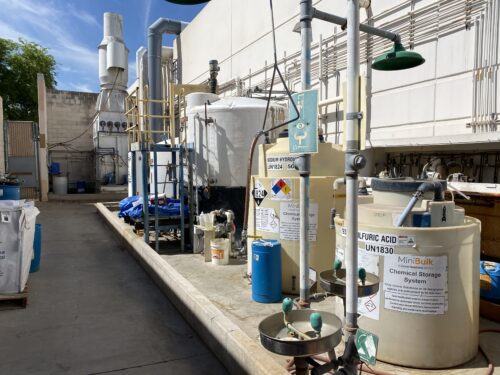 For a semiconductor equipment cleaning company, success had started to create an unexpected problem.
Demand for their cleaning and refurbishment services was growing—but their wastewater treatment system couldn’t keep up. What had once been sufficient had become a daily bottleneck: an undersized, fully manual process struggling to handle increasing volumes of highly variable, chemically complex wastewater.
Each cleaning cycle generated bursts of aggressive waste streams—strong acids like nitric, sulfuric, and hydrofluoric, alongside caustics such as sodium and potassium hydroxide. These streams carried valuable, but challenging-to-remove metals like copper, silver, and gold. Treating them required careful chemical dosing, pH adjustment, and solids separation.
But everything was manual.
Operators physically handled chemicals, measured and dosed them by hand, and managed each batch step-by-step. The process was slow, labor-intensive, and raised clear environmental, health, and safety concerns. Treatment cycles stretched longer than they should, limiting throughput and putting pressure on operations.
Then came another challenge: an upcoming discharge permit change that would require fluoride removal—adding yet another layer of complexity to an already strained system.
The company explored outsourcing the problem through offsite disposal. But the costs quickly made it clear—this wasn’t a sustainable path forward.
If they wanted to grow, they needed to rethink everything.
THE SOLUTION
 Rather than jumping straight to equipment, Anguil partnered with the client to step back and fully understand the operation: how often waste was generated, in what volumes, and how it varied from batch to batch.
That insight shaped everything.
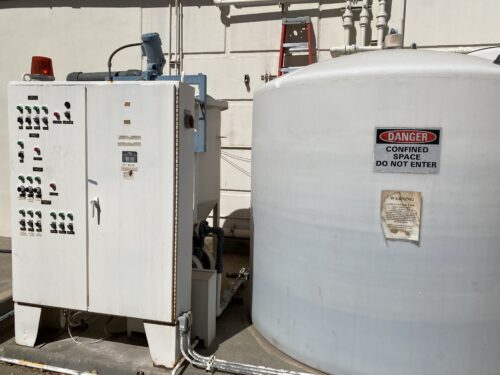
With limited outdoor space available, simply “scaling up” wasn’t an option. The solution had to be smarter, not just bigger. Anguil’s engineers worked alongside the facility team to reimagine how the system could fit—designing tall, high–aspect ratio tanks that made use of vertical space instead of expanding the footprint.
At the same time, treatment chemistry was evolving. Working closely with the client’s chemical engineers, Anguil helped validate an updated process that incorporated fluoride removal through lime softening—ensuring compliance with future discharge requirements without compromising efficiency.
Different approaches to solids handling were also evaluated. While advanced technologies like rotary vacuum drum filtration were considered, the team ultimately selected an upgraded filter press—balancing performance with budget realities.
Every decision was made collaboratively, grounded in both technical performance and practical constraints.
The final system transformed what had been a manual, reactive process into a streamlined, automated operation.
Separate equalization tanks now isolate acidic and caustic waste streams, preventing unwanted reactions and stabilizing incoming flows. From there, wastewater is automatically transferred into a central reaction tank, where treatment programs are executed at the push of a button.
Chemical addition, pH adjustment, metals precipitation, and fluoride removal all occur in a controlled, repeatable sequence—eliminating the variability and labor demands of manual operation.
Even the physical layout was designed with efficiency in mind. A custom elevated platform allows the filter press to discharge dewatered solids directly into a dumpster below, simplifying handling and reducing operator involvement.
Behind the scenes, a PLC-based control system ties everything together, while a user-friendly interface gives operators clear visibility and control without requiring constant intervention.
To accelerate installation, much of the system was pre-assembled on skids—minimizing field work and enabling a faster, smoother startup.
THE RESULT
The impact was immediate—and measurable.
What had once been a constraint on the business became a catalyst for growth.
- Treatment capacity doubled
- Weekly batch throughput tripled—from 3 to at least 9 batches
- Manual labor requirements dropped by over 80%
- Operators were removed from routine chemical handling, improving safety
With the new system in place, the company could confidently meet demand, operate more efficiently, and plan for future growth—all while staying ahead of regulatory requirements.
At its core, this project wasn’t just about wastewater treatment. It was about aligning a technical solution with real business goals.
By taking a collaborative, step-by-step approach—grounded in data, validated through testing, and refined through open dialogue—Anguil helped turn a complex operational challenge into a long-term advantage.
Because the best wastewater solutions don’t just treat water.
They unlock capacity, reduce risk, and move businesses forward.
A Practical Path to Wastewater Compliance
Comments Off on A Practical Path to Wastewater ComplianceTHE CHALLENGE
 When a subsidiary of a global manufacturer of spray‑dried natural ingredients learned that its municipal wastewater discharge permit was about to be updated, leadership knew action was needed—and quickly. The new permit would impose tighter limits on pH, solids, organic loading, and discharge flow, creating both operational and financial risk for a facility already operating within tight physical and budgetary constraints.
The company had a strong track record as a responsible community partner and wanted to stay ahead of potential violations. To explore their options and avoid unexpected fines—or worse, a shutdown of wastewater discharge—they turned to Anguil for help.
Early conversations made one thing clear: pH compliance was non‑negotiable. The city made it clear that a single pH violation would trigger an immediate notice of violation, followed by steep fines and possible suspension of discharge privileges.
Unfortunately, this facility produced wastewater across one of the widest pH ranges Anguil typically encounters. Tomato- and vinegar‑based process streams come in around pH 3, while CIP operations introduced short bursts of wastewater with pH as high as 12–14. Any solution would need to reliably handle both extremes—automatically and without fail.
At the same time, the facility’s discharge flow told a story of its own. For most of the day, flows were below 100 GPM. But during CIP events, wastewater surged to more than 400 GPM in a short window. The updated permit, however, capped discharge to the city sewer at 100 GPM due to upstream capacity limitations.
As Anguil dug deeper, additional constraints surfaced:
- Wastewater contained elevated TSS, ammonia, and BOD
- The city required 100% secondary containment for 30,000 gallons of glacial acetic acid stored onsite
- The site had almost no available real estate for new construction
- Existing sumps commingled industrial wastewater with sanitary flows, which would need to be corrected
It was clear this wasn’t just a treatment challenge—it was a systems challenge.
THE SOLUTION
 Anguil worked closely with the client to quantify the real-world impact of the updated permit. Together, they evaluated the cost of violations and surcharges, the capital required for various treatment options, and the likelihood of corporate approval for major investments.
Technically, Anguil could design a system to reduce TSS, BOD, and ammonia using a dissolved air flotation (DAF) system and sludge dewatering. But when the numbers were put on the table, the return simply wasn’t there. Paying municipal surcharges for ammonia and residual BOD made more financial sense than installing and operating a full treatment train.
What did make sense was eliminating the risk of violations altogether and controlling discharge flow—while keeping capital costs in check.
Anguil initially developed a comprehensive treatment concept, including storage, pH adjustment, DAF, and a new treatment building. But geotechnical studies revealed that foundation work alone would drive costs well beyond what corporate leadership was willing to approve.
Rather than forcing a one-size-fits-all solution, Anguil recalibrated.
By listening closely to corporate feedback and site constraints, Anguil helped the client refocus on what mattered most:
- Guaranteed pH compliance
- Flow equalization to meet the 100 GPM discharge limit
- Sufficient storage to manage both process variability and secondary containment requirements
- A design that fit within the existing site and allowed future expansion if needed
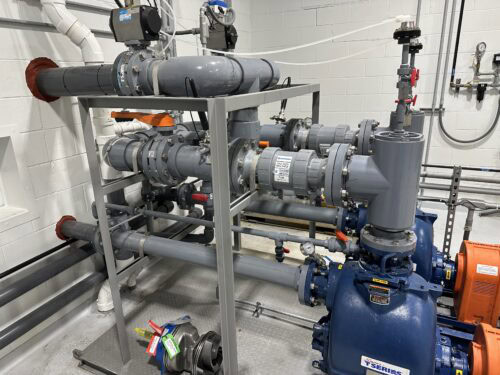
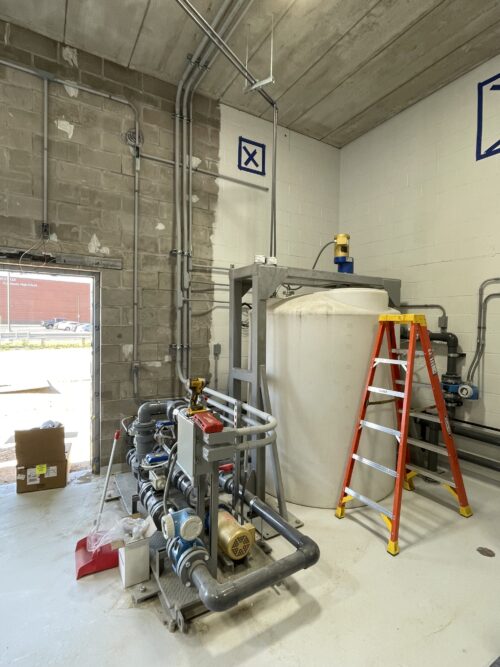
The final solution was a fully automated pH adjustment and flow control system, built around:
- A new dedicated process wastewater sump
- Approximately 80,000 gallon storage capacity in FRP tanks installed outdoors
- Continuous pH adjustment with mixing, and chemical dosing
- PLC-based automation with VFDs, alarms, and remote access
- Bench testing to confirm chemical dosing rates and operating costs
By repurposing space inside the existing production building and avoiding new foundations, the customer dramatically reduced capital costs while still meeting all critical permit requirements.
THE RESULT
Anguil collaborated closely with the customer and their third-party engineer to finalize layouts, instrument placement, and sump integration. Equipment skids were fabricated, leak-tested, and delivered ready for installation. The customer’s maintenance team handled field installation, while Anguil supported commissioning and startup.
Once online, the system performed exactly as intended. Automated controls minimized operator involvement, and remote access allowed Anguil engineers to fine-tune performance during commissioning. Real-time alerts and reporting gave the operations team confidence that compliance was being maintained around the clock.
In the end, the customer achieved exactly what they needed:
- Reliable pH compliance, eliminating the risk of violations and shutdowns
- Controlled discharge rates, fully aligned with municipal constraints
- A significantly lower capital investment than originally anticipated
- Automated, low-touch operation that reduced staffing demands
- A flexible platform that can support future treatment upgrades if regulations or business needs change
By taking a holistic, collaborative approach, Anguil helped the client navigate a complex regulatory challenge without over‑engineering the solution—delivering compliance, confidence, and long-term value.
Onsite Wastewater Treatment for an On Point Budget
Comments Off on Onsite Wastewater Treatment for an On Point BudgetThe Challenge
A global manufacturer of key chemical ingredients used in a wide array of products including clothing, carpeting, automobile thermoplastics, computer cases, and sporting equipment, was planning a facility relocation and expansion that presented a significant wastewater treatment challenge.
At their previous location, the manufacturer was using a perozone system to treat their cyanide-laden wastewater. However, the system as designed could not meet the rigorous discharge standards of the local Publicly Operated Treatment Works (POTW) on the order of 0.04 ppm. Further, they had abandoned the peroxide injection system to reduce the health and safety risks per a companywide mandate.
The expansion required a relocation to a new facility, but the increased production would also triple the company’s wastewater volume. If they did not find an onsite treatment solution, the hauling and disposal costs were going to dramatically increase operating expenses.
The Solution
Nailing Down the Requirements
Anguil collaborated with the client to understand their specific challenges and determine the project objectives. We gathered benchmark data at the existing facility to identify possible solutions that offer the best return on investment (ROI). Project engineers then worked with the customer to understand their decision-making criteria to evaluate only business viable treatment approaches.
In this case, the client’s priority was to eliminate hauling and disposal costs of their cyanide-laden wastewater. With the expansion at a new facility, they expected their wastewater volume to triple, as well as the corresponding disposal costs. Secondly, they wanted a fully automated system with minimal operator intervention so they could focus on producing products. Third, they wanted to minimize the storage and handling of any noxious chemicals.
Next, water samples were sent to the Anguil lab to validate the different technology considerations. Anguil typically identifies several potential treatment and process options which align with the client objectives, and after presenting these to the customer, collaboratively selects one or several to validate. Anguil proposed several oxidation schemes. The client preferred to move away from ozone and peroxide so alkaline chlorination was selected for this project. It is a well-known method with wide application to similar waste streams and is easily automated.
To validate the treatment process, the customer elected for both a bench trial as well as a scaled pilot. For the bench work, the client provided 5 gallons of wastewater collected from their existing facility. Using the required caustic and bleach treatment protocol and measuring free HCN content via the USEPA Pyridine Barbituric Acid Method (Method 10265), test samples were returned which were below the POTW limit of 0.04 ppm. Based on the bench tests results, chemical dosing requirements and costs were easily established before the system was even installed.
Bench Verification
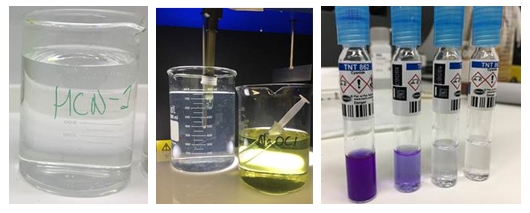
Figure 1 – As received waters from the two (2) drums of HCN wastewater marked 1 and 2 respectively. (Right) HCN wastewater post treatment.
Figure 2 – Example HCN measurements. Non-detect is shown on the right, over range on the left.
After the validation that the method would work, albeit on small sample volumes, the customer requested that Anguil perform a larger pilot study to both validate that larger batch treatments would perform similarly. For the pilot work, the client sent Anguil two (2) fifty-five-gallon drums of wastewater. Adapting an existing pilot system, the same reactions were performed at the previously determined set-points on 15- and 25-gallon batches. Again, final concentrations of HCN were below the required discharge limit. In addition to the further treatment efficacy validation, the chemical dosing requirements were used to estimate yearly operational expenses for the full-scale treatment system as well as size and design the required chemical reagent storage capacity.
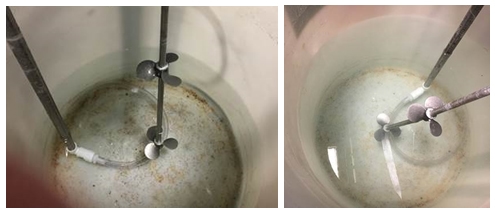
Figure 3 – Appx 15 gallons of HCN wastewater before treatment (left) and after treatment (right). Again, the cloudiness is due to the formation of the precipitate.
Putting it all Together
The final step in the process is the system design, realization, and installation. Anguil put together the proposal for a fully automated batch treatment system to handle their expected treatment volumes. The proposal contained specifics on many mechanical components including the tank, pumps and mixer sized as well as the advanced automation and controls – including integration with their existing infrastructure and DCS system – to meet their requirements. Additionally, the appropriate service options for installation, installation supervision, commissioning, and training were included. After the system was installed, Anguil performed a 3-day start-up and training including verification of the system’s ability to treat the wastewater. Anguil’s Aftermarket team will be there to service and support the client as needed.
The Result
Anguil’s approach to solving a client’s wastewater problem is to take a wholistic view of the challenge with a series of go/no go steps throughout the process. Project Engineers are always focused on the customer’s business objectives in a collaborative effort to define an efficient and cost-effective trial to validate treatment approaches that align with their objectives. Through the bench and pilot testing, we offer insight gained along with a comparison of pros/cons of the treatment approaches until we get to the treatment system that aligns with the client needs.
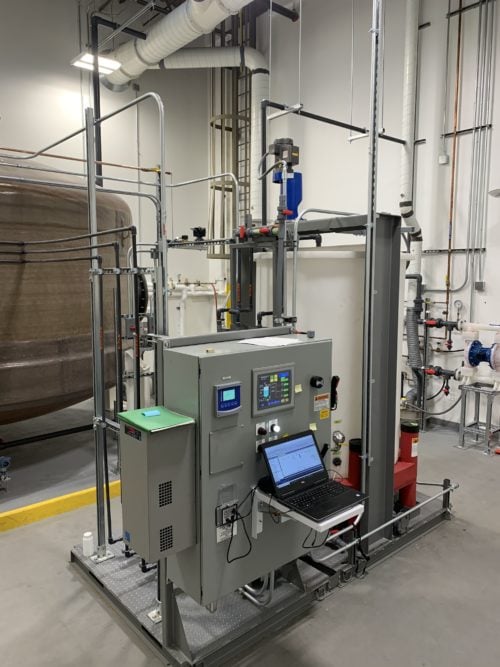
As a system integrator with 35+ engineers and 60+ supporting personnel, we take a technology agnostic approach to help our clients get the system they want. In this case, the results from our effort:
- Client walked through a collaborate process to ensure key decision criteria and objectives were met in a timely and cost-effective manner.
- Customer was able to evaluate various oxidation treatment options that aligned with safety and cost parameters.
- Lab and pilot validation trials confirmed treatment approach and provided operational expense estimates to client as requested.
- Anguil provided a single-source system integration approach that included all engineering (Mechanical, Electrical, CAD, Project Engineering) and support services in-house to mitigate exposure to risk and deliver a fully integrated system with install, commissioning, and training support.
- The treatment approach saved the client considerable amount of money versus hauling and disposal services; providing an ROI estimated in the 14-16 month range.
- Anguil’s electrical engineering team developed the automation and controls to automate the batch-treatment process. This results in minimal human interaction and an extremely efficient process. It also proactively notifies them via text and email of system condition, need for chemical reorder, reporting and remote login capabilities.
Note: At the time of bench and pilot testing this wastewater, Anguil was engaged with a second wastewater produced by the client. We followed a similar approach and validated treatment efficacy through lab and pilot studies. The result of onsite treatment for both wastewaters offered the client an incredible cost savings with minimal impact to resources.
Frac Water Reuse Technologies
Comments Off on Frac Water Reuse TechnologiesTHE CHALLENGE
The worldwide energy sector has accelerated the development of its unconventional oil and gas resources through increased use of horizontal drilling and hydraulic fracturing practices. Water is an essential element in the fracturing process and the recycling or reuse of spent water can dramatically reduce costs. The volume of water required to fracture a well varies, but it generally ranges from one million gallons to five million gallons. Operators face difficult challenges securing water sources for their operations, especially already dry regions. Furthermore, the management of waste water associated with hydraulic fracturing has an environmental impact and associated cost.
The development of technology to recycle and reuse this water is now becoming critical and Anguil has integrated solutions to help. We have developed an effective water recycling system that allows well operators to safely reuse water without jeopardizing well output.
THE SOLUTION
Water Recycle and Reuse
Water generated during drilling, well completion, and production is categorized either as flowback or produced water. Flowback water is the initial fluid produced after hydraulic fracturing and is typically recovered during the first six weeks of well production. The flowback water characteristics stem from the initial source water, the natural formation brine, fracturing fluid additives, proppants, and drilling fluids. Generally, 20-40% of the fracturing fluid volume is recovered as flowback. Produced water is the water which naturally exists within shale formation and is recovered concurrently with oil and gas. After the initial flowback period, produced water resembles the characteristics of the formation brine. The volume recovery rate of produced water is lower in comparison to the flowback, but occurs over the decades of a well’s lifetime. Currently, the majority of flowback and produced water is disposed of in salt water disposal wells.
Recycling and reuse of flowback and/or produced water reduces fresh water demand and the associated costs of water purchase, transportation, and disposal. In contrast to the usual practice of complete disposal, a portion of the flowback is treated for reuse either onsite or at an adjacent well. The primary economic benefit from recycling is a significant reduction in the number of truck loads required to ship fresh water to the well site and the flowback water offsite. Environmental benefits include reduced reliance on and competition for fresh water sources, a reduced carbon footprint from trucking, and less stress on the local infrastructure.
Treatment requirements for flowback and produced water are normally established by the company performing the well completion. Knowledge of the fracture fluid employed is required when considering the recycling methodology in order to identify the required treatment characteristics. Two common fracturing fluids are slick water and gels. Slickwater is normally used for natural gas production, whereas gels are often deployed for oil field development.
Anguil’s Frac Water Reuse System
Since there is a wide variation in flowback and produced water quality in oil and gas fields, Anguil Aqua Systems is presently focused on the treatment of flowback and/or produced water from natural gas wells.
Previously, the high levels of Total Dissolved Solids (TDS) in produced water were thought to render it unusable. However, well service companies have demonstrated that moderate TDS levels in recycled water do not impact well production capacity. Hence our solution is to focus on the minimization of Total Suspended Solids (TSS) and, overall reduction of bacteria and other contaminants affecting the fracturing fluid additives.
Of the many approaches to the minimization of TSS, the Anguil solution is a ballasted flocculation system. Similar systems have been successfully employed to treat drinking water as well as municipal and industrial waste waters containing many of the same contaminants found in flowback and produced waters.
System Description
 The diagram at right depicts the flow pattern for the clarification process. In the first tank, the raw water or influent is combined with a coagulant, commonly ferrous sulfate, ferric sulfate, ferric chloride, or alum. The coagulated influent then passes into the flocculation tank where a polymer and a ballast material such as microsand, iron oxides, or chemically enhanced sludge is added. Coagulation and sedimentation times are reduced by the addition of chemical additives and the ballast material. After ballast and polymer additions, the flocculated water then proceeds to the third tank where additional mixing occurs, allowing the floc to coalesce into larger precipitates. The matured, flocculated water proceeds to the clarification tank where the floc is separated from the water by passing through plate or tube settlers. Clarified water then exits from the top of the system.
Settled floc and ballast material are collected and pumped to the ballast recovery unit where the ballast is separated from the waste solids. The waste solids are sent to disposal and the recovered ballast is returned to the first flocculation tank. We can provide treatment systems which help improve injection facilities operations and maintenance, reducing injection pressures and minimizing acid jobs by keeping your wells from fouling. Furthermore, our solutions include treatment options to enhance your oil recovery and treat for hydrogen sulfide control.
THE RESULT
As a member of the Gas Processors Suppliers Association, Anguil is heavily invested in industry’s success and future. Countless air pollution control installations at natural gas processing and petroleum refining sites gives us the necessary knowledge to address your water treatment needs safely, effectively and within your demanding production schedules.
- Reuse of Flowback and Produced Water: Physical and chemical treatment system that reduces suspended solids to acceptable reuse standards for hydraulic fracturing.
- Mobile Precipitation: A system easily deployed on site, allowing treatment for multi-well completions, or transport to a nearby well.
- High Contaminant Removal: Total Suspended Solids (TSS), turbidity, oil/grease, color, and bacteria.
- Chemical Coagulation: A wide range of available coagulants and polymers allows customization to site specific needs.
- Automated Chemical Feed System: Treatment begins with proper dosing of chemicals to precipitate dissolved contaminants. The Frac Water Reuse System incorporates chemical metering pumps, day tanks and pH instrumentation to ensure treatment objectives are being achieved.
- Lower Costs: Ballasted clarification allows for smaller equipment footprint, reduced power consumption, and reasonable chemical use. Recovery and reuse of ballast material lowers consumable costs.
- Short Term Lease Agreements: Flexibility to only pay for water recycling system during peak water demand.
- Customized Service and Project Management Contracts: Anguil personnel can be contracted to provide continuous service and/or operation of the entire water recycling system.
Wastewater Compliance Techniques For Food Processors
Comments Off on Wastewater Compliance Techniques For Food ProcessorsTHE CHALLENGE
Food production is a demanding and competitive process. Executives are continually confronted by product development processes, competitors, and deceptive practices for economic profit. In today’s environmentally aware climate, reputation is crucial. Producers worry they could be perceived as environmentally and socially irresponsible. If they are, some retail chains may refuse to stock their brands until they make extensive, and often expensive changes.
Many producers are facing a new, and unexpected, complicating factor: failing and undersized Publicly Operated Treatment Works (POTWs). Wastewater previously discharged with little processing may now be subject to surcharges. Publicly Operated Treatment Works struggle to meet increased Environmental Protection Agency (EPA) regulations, while making infrastructure improvements to accommodate the greater load.
Another obstacle: treatment system operators, with decades of experience, are retiring. Unfortunately, the knowledge of how to run their outdated treatment system retires with them. This leaves system owners and executives wondering how to replace that knowledge base while meeting new regulations.
In the face of increased regulatory control, rising environmental concerns about wastewater, and a retiring workforce, food producers are seeking cost-effective ways to stay in compliance.
THE SOLUTION
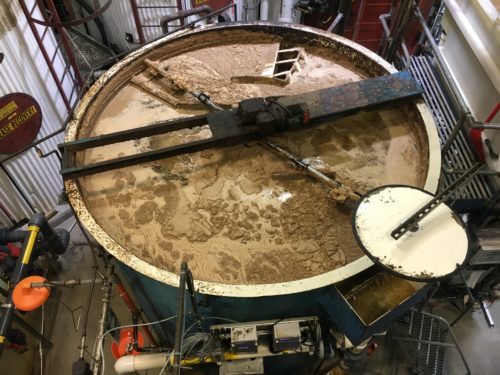 Anguil Environmental provides highly engineered equipment and service solutions that solve complex industrial air and water concerns. Anguil follows a very simple, but effective, four-step approach that addresses economic, operational, and compliance challenges.
The first step is to evaluate the situation and parameters. We collaborate with the client to understand their challenges and determine the project needs and objectives. We gather benchmark data to assist with alignment of solutions that offer the best return on investment (ROI), then work with the customer to understand their decision process and criteria to ensure we can fulfill all their requirements.
The second step is exploring all treatment and operational processes in the Anguil lab. Anguil confirms all potential treatment and process options that align with the customer objectives. This step involves wastewater samples in our in-house wet lab to validate potential treatment protocols.
Testing in-house provides on hand data for evaluation of viable treatment options, which is then used to generate a simple Process Flow Diagram (PFD) to illustrate the equipment needed to meet customer parameters.
The third step is placing a pilot system onsite to test waters. With the client satisfied with our lab trials, we ask if they require a pilot system to validate the treatment approach in normal conditions onsite.
THE RESULT
The fourth, and final step in the process is commercial deployment. After completion of lab testing, discussion of various equipment options and testing against the business case, Anguil provides a firm proposal for a treatment system which would meet the treatment efficacy and business needs of the customer. The proposal contains detailed information on the treatment system, estimated operational costs, and options for installation, start-up, and commissioning. The flexible approach allows the customer to choose the package that best suits their needs. Additionally, Anguil’s Aftermarket and Service group is proactively in touch, ready to provide long-term system, and parts support.
Anguil follows a better approach to solving complex water challenges, which starts with listening to the client’s needs and business case. Anguil advocates an efficient process that would provide the client with the information they want to make an informed decision.
Single Source For Success
Comments Off on Single Source For SuccessThe Challenge
A packaging company who had traditionally manufactured steel cans decided to diversify by adding aluminum aerosol cans to their product portfolio. Due to the extensive project scope and a significant capital investment in new equipment including air and water pollution control, the packager stipulated that the successful vendor had to single source the entire project. Since the can making equipment manufacturer who ultimately won the project was not an expert in air and water treatment, they in turn searched for a partner with the ability to single source all pollution control aspects. Anguil, a single source air and water treatment system provider, was selected to be that partner.
The Solution
NAILING DOWN THE REQUIREMENTS
The aluminum can making process requires water to remove oils and post-forming debris as well as chemical surface conditioning of the cans to prep for coating. To accomplish cleaning and conditioning, the cans are passed through a large multi-stage washer, which 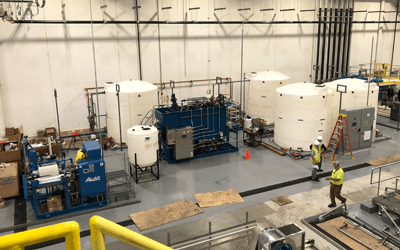 requires clean, consistent input water. Concurrently, the dirty rinse water needs to be pretreated before it can be discharged to the local Publicly Operated Treatment Works (POTW). Since this was a new line for the equipment manufacturer, Anguil assisted the manufacturer with developing specifications for:
- Input water quality (conductivity < 10 micro Siemens)
- Average input flow (30 GPM)
- Required washer input pressure
- The need for a “fast fill” mode to quickly refill the washer after maintenance activities
- The requirement for maximal equipment up time
With customer input, Anguil selected a dual train Reverse Osmosis (RO) system to meet the washer’s influent requirements.
On the wastewater side, where the exact water chemistry was unknown, Anguil again worked with the can manufacturer to determine an expected range of water contaminants to select candidate treatment technologies which could handle the variable chemistry. Expecting a pH of 2-5, high TSS loading, significant amounts of sulfuric and hydrofluoric acids, oils and greases as well as possible surfactants, Anguil proposed a form of enhanced clarification called Ballasted Flocculation (BF). With a BF system, the pH could be adjusted as needed, fluoride and other metals precipitated, and oils broken out of suspension chemically using caustic addition, coagulants and polymers. With the addition of sand to flocculated species, the settling rate increases dramatically, leading to a smaller overall equipment footprint, important since this wastewater treatment system was to be housed inside the production facility. Extra space was left in the system design to allow the addition of water polishing equipment if after start-up, it was deemed necessary.
Because Anguil is an air and water treatment supplier, Anguil was able to evaluate solutions for both treatment needs, ultimately proposing a solution that did not require air pollution control equipment. Again, this fits into Anguil being a technology agnostic solution provider always on the look-out for the customer’s bottom line.
PUTTING IT ALL TOGETHER
After determining the flow and treatment requirements for the Process Water Conditioning System (PWCS) and the Wastewater Treatment System (WWTS), Anguil proceeded to determine the required logistics equipment and controls to operate both systems in automatic mode with the least operator involvement possible.
For example, inlet water buffer and RO permeate storage tanks were selected to supply some onsite storage, ensuring back-up capacity should the city water supply fail and to provide constant, even flow to the varying washer demands. Non-metallic AODD pumps were selected to lift and convey the high solids content and corrosive waste water to the treatment system. An equalization tank and an emergency dump tank were included to buffer flow through the WWTS while providing emergency capacity if the washer needed to be dumped for maintenance reasons, and to collect additional waste water sources from sludge dewatering and secondary containment floor sumps.
In addition to the mechanical components of both the PWCS and WWTS, Anguil’s control engineers worked to integrate both the larger sub-systems (RO, ballasted floc, Rotary Vacuum Drum) into the treatment plant. More importantly, they also worked directly with the canning equipment manufacturer to seamlessly integrate the disparate washer/water treatment systems to minimize production downtime and product loss in the event of failures with the PWCS, washer system or the WWTS.
GETTING THE SYSTEM UP AND RUNNING
After obtaining customer approval of the system design, Anguil ordered the long lead-time items, namely the tanks and large third-party vendor skids. Once these items were on order, Anguil coordinated the purchase and delivery of all the parts (pumps, valves, instrumentation, etc) to be shipped loose for field installation or to be assembled on Anguil pump skids.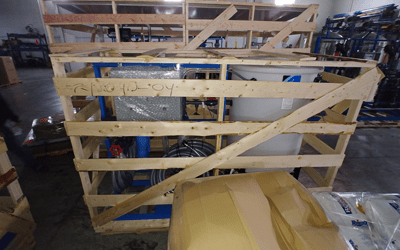
Since the canning equipment manufacturer had already obtained the services of installation contractors, Anguil was not engaged for a turn-key installation. However, based on our installation experience with similar systems, Anguil received, labeled each part with its PID drawing tag number, and then “kitted” all the parts into boxes to aid the installation process. For example, all the instruments, valves and piping fittings associated with a given storage tank or sub-assembly were placed in their own box. Kitting parts in this way acted as a quality control step, ensuring the correct parts and amounts were delivered, and greatly assisted the install crew as they knew exactly where and how many parts to install on each tank.
Even though Anguil was not asked to perform installation work, Anguil was hired to provide an install supervisor to interface with contractors, provide guidance where necessary, troubleshoot issues, expedite defective part replacement, communicate the project schedule and handle changing project requirements. One direct benefit of Anguil’s install supervision was the ability to respond rapidly to changing site conditions and requirements. For example, prior to processing cans, the washer system required a “passivation” step consisting of treating the washer interior with caustic and acidic waters. This requirement was not originally intended to be included in Anguil’s scope in any way. However, to assist the customer, Anguil reorganized the installation effort to enable the RO system to be run in manual mode to feed the washer and the wastewater treatment system to be run in manual mode to allow discharge and pH neutralization of the passivation water.
Special site supervision and controls workarounds were required since the equipment had not been fully commissioned and installed at the time passivation was to occur. However, Anguil’s ability to accommodate the project needs saved the customer $100,000s in disposal and transport costs of the passivation water. After can making equipment was brought online, Anguil brought in their commissioning crew to ensure that the control program was operating correctly – especially with communications between the PWCS, WWTS and washer system. This included confirming that chemical protocol was validated and optimized and ensuring that any issues discovered during the initial start-up and shake-down were addressed quickly and efficiently. Ultimately, after training the site personnel on the system operation, troubleshooting of general issues and becoming familiar with system operation, both the PWCS and WWTS were able to support the washer’s input and waste water needs with minimal operator involvement and get the packager back to what they do best—making cans.
The Result
- Anguil was able to walk the customer through a collaborative treatment technology selection process resulting in systems (waste and process) that the customer was comfortable with and had high confidence would meet the desired treatment efficacy.
- Anguil’s approach of sticking to our core competency of engineering and integration led to the selection of technologies and vendors which resulted in a successful water treatment system.
- Anguil’s single source approach enabled streamlined communication when problems arouse. Instead of the customer calling multiple vendors, trying to figure out who owned the problem, they would call Anguil and Anguil led the charge as necessary. One call did it all.
- Anguil’s ability to provide both air and water treatment solutions allowed our engineering experts to explore all possible solutions and design the best fit treatment train — which ultimately removed the need for air pollution control—and lowered the total cost of ownership of the treatment system.
- Even though the customer had already contracted with installation contractors for this project, Anguil’s experience with turn-key installations made it apparent that the logistics of kitting equipment was necessary to ensure project success—all conducted within the original contract price.
- Because of the amount of pre-work done scoping the customer’s needs for both the PWCS and WWTS, no change orders were issued to complete the work—except for those items requested by the customer at a later date.
- Anguil’s customer-focused philosophy enabled us to maintain a flexible schedule to accommodate rapidly changing site demands without significant added costs to the customer.
Industrial Wastewater Treatment
Comments Off on Industrial Wastewater TreatmentThe Challenge
Anguil Environmental Systems was asked to supply an oxidizer and packed tower air stripper to treat a 65 gallon per minute water stream containing significant concentrations of Diesel Range Organics (DRO), Volatile Organic Compounds (VOCs) and Total Suspended Solids (TSS). The customer was sending the wastewater stream through a cooling tower which was continually fouling from the DRO present in the water. Significant maintenance costs and production downtime were incurred every time the tower was being brought out of service for cleaning. In addition, the customer was trying to achieve zero VOC emissions from their facility.
The Solution
Application engineers at Anguil determined that a Regenerative Thermal Oxidizer (RTO) would meet the customer’s needs but were skeptical that the air stripper would function properly given the customer supplied water characteristics. Anguil was engaged to evaluate the water stream for the air stripping application. Review of the supplied water analysis indicated that concentrations of the heavier Diesel Range Organics (naphthalene and higher) were beyond their solubility limits. Hence, the presence of free product in this water stream would quickly cause any air stripper to foul, detrimentally impacting stripping performance and potentially creating a safety hazard. Anguil recommended that the customer evaluate oil/water separation and emulsion breaking to remove and potentially recover the free product prior to entering the air stripper.
The Result
Using water samples obtained from the customer, an initial bench evaluation of oil/water separation was conducted. Upon receiving the samples, Anguil realized that either the customer-supplied water analysis was incorrect or that the water samples received were not representative of the customer’s process water since the presence of free product was not observed. The emulsion breaking tests were performed anyway, predictably meeting with little success. In addition to the emulsion breaking tests, Anguil attempted to coagulate the water to determine if this approach would be suitable, determining this method had merit.
Based on results from the initial separation study, Anguil recommended two courses of action. First, the customer would redo their analytical water analysis using suggested test methods to improve confidence in the treatment design requirements. Based on the results of the second round of analytical tests, Anguil suggested that a two stage pilot study be conducted. For Stage 1, Anguil representatives would perform treatability studies on site via jar testing. Based on the results obtained from Stage 1, Anguil engineers would perform a full scale, onsite pilot with the appropriate equipment for Stage 2.
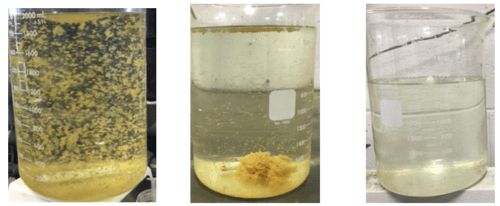
Stage 1: Anguil representatives traveled to the site and performed jar tests directly with the process water in question. Since the process water was at a temperature of 110-120 oF, it was advantageous to work with the process directly rather than trying to ship samples off site possibly compromising their integrity from cooling, biological action or chemical reactions from long hold times. After a number of trials, they successfully determined that the water could be coagulated by raising the pH from 4 to 8.5, utilizing a poly aluminum chloride (PAC) based coagulant blend and a standard polymer. After coagulation and filtration, color, turbidity and solids content were reduced. Anguil then sent the untreated and treated water for third part lab analysis to determine the overall effectiveness of the process. The results were promising and the customer elected to move forward with Stage 2 of the pilot study.
Stage 2: Based on the site constraints and treatment goals, Anguil modified its pilot clarification system to perform the second stage of the study. Equipment arrived onsite,was unloaded and placed within the facility. A generator was rented since the facility could not easily supply the required power. Anguil then proceeded to unpack and plumb the pilot system into the existing process piping.
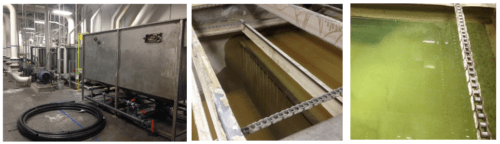
Once everything was set-up, pumps primed and running, the operator filled the tank with process water and began processing using the chemical formula determined in Stage 1: Raise pH > 8.5 using 50% caustic solution, add 300 ppm coagulant, add 1 ppm polymer. As expected, the clarifier influent demonstrated a good floc which quickly began to settle to the bottom of the clarification tank. With continued processing, clarity improvements in the clarification tank became noticeable as submerged parts of the tank became visible as the initial dirty water was displaced by the coagulated and clarified water. Water samples pulled from the clarifier effluent were obviously cleaner than the raw process water, and with continued processing acceptable clarity was achieved.
After successfully demonstrating the clarification process, treated samples were pulled and tested using the same test protocol used in Stage 1. In addition, a sludge sample was sent for benzene analysis in order to determine if the sludge would be considered hazardous. Sludge production rates were quantified by coagulating, flocculating and filtering specific volumes of process water. Filtered samples were wrung dry and air dried for several days. Wet and dried samples were weighed.
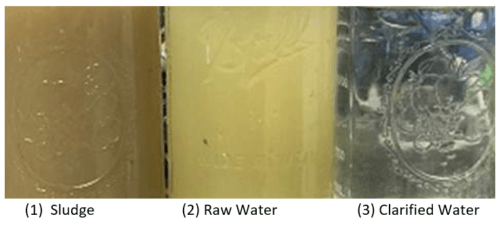
The qualitative and quantitative results met the customer’s expectations and treatment goals. The chemical coagulation protocol and clarifier in this pilot work were able achieve a DRO reduction of 85% or greater and an 80% reduction in TSS. Since Anguil was proposing a ballasted floc system for the final treatment system to handle the design flow rate of 65 GPM, another set of samples was taken for ballasted floc testing which achieved similar DRO removal rates but improved on the TSS reduction to less than 1 NTU. After reviewing the sludge production rates and potential hazardous classification for the sludge, the customer asked Anguil to recommend a sludge dewatering system. Further, after reviewing the treatment system capabilities and facility requirements, Anguil recommended removing the air stripper and oxidizer from the scope of supply as it was determined that removing the heaviest organics would solve the facilities heat exchanger fouling problems, and the limited VOC loading did not justify the use of an oxidizer.
Anguil was able to guide the customer through the equipment design and selection process by identifying and rectifying shortcomings in the analytical data, avoiding time and cost specifying and designing equipment which would not address the customer’s project goals. Ultimately, the main benefit of Anguil was determining a solution which did meet the customer’s objectives despite the fact that the selected solution differed greatly from the original request. Onsite jar and pilot tests allowed the customer to become educated and familiar with the treatment process while understanding the benefits, capabilities and trade-offs of the proposed system. Further, being on site allowed Anguil to really understand the customer’s needs and process, allowing them to identify customer process variables which could potentially affect treatment system performance and provide seamless integration of the new treatment system into the existing process.
Superfund Site, Water Pump & Treat
Comments Off on Superfund Site, Water Pump & TreatThe Challenge
Anguil was contracted as part of a team of companies to implement a groundwater pump and treat system intended to remove trichloroethylene (TCE) from a local aquifer designated as a Superfund Site by the Environmental Protection Agency (EPA). Though the site is nestled between the buildings and roadways of 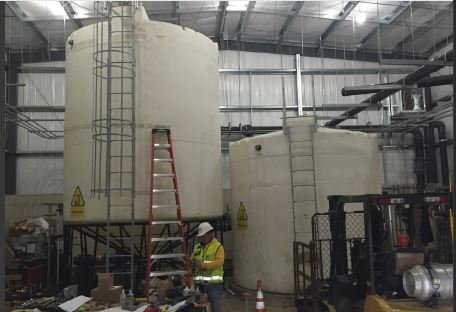 an operating industrial facility, the overall extent of the pump and treat system is expansive. Extraction wells are located over 1,000 ft. from the treatment building, with an additional 1,200 ft. of pipe run to the injection wells. All of the water treatment equipment and main control system were designed to be contained within the new treatment building, while control panels located at the extraction and injection areas were to provide local control and monitoring of the appropriate wells. Everything was to work seamlessly together.
The 500 gallon per minute (GPM) pump and treat system, as well as the overall site plan, were designed by a large engineering, procurement and construction (EPC) firm working on behalf of the responsible party. A general contractor and dedicated installation sub-contractor were selected to prepare the site, drill the extraction and injection wells, install the underground conveyance piping, erect the prefabricated treatment building, install the treatment equipment and perform all the interconnecting piping.
The Solution
Anguil was contracted for two phases of this project. During the design and approval portion, Anguil’s Electrical Engineering and Controls team was asked to review the electrical design and system controls. In addition, Anguil EEs also provided and reviewed the system controls specifications to facilitate approvals from the EPA and Army Corps of Engineers. For the construction phase, Anguil provided and managed the delivery of all the water treatment and water logistics equipment, including the control system and control panels. Furthermore, during the construction phase, Anguil field service engineers provided installation and shakedown assistance for the entire system.
Anguil’s scope of supply included all valves, process instruments and transmitters, water treatment equipment, the exhaust stack, storage tanks, pumps, chemical injection system, motor control system, main building control panel as well as two remotely located panels at the extraction and injection well sites. Further, to the largest extent possible, Anguil was directed to supply the equipment skid mounted, pre-plumbed and prewired.
The Result
Anguil was able to bring additional value to this project by successfully managing the multiple vendors of both the water treatment and controls equipment for the EPC. In particular, Anguil identified low-cost, expedited options to meet the aggressive construction schedule mandated by the EPA penalty deadlines, in some cases cutting long lead times in half. Having a custom solutions integrator on this project was especially valuable when major, unforeseen factory delays occurred. By effectively communicating with the construction team, schedules and resources were adequately adjusted. Further, Anguil was able to manage discrepancies between the selected vendor’s products and customer specifications, achieving the design specifications without sacrificing performance.
Throughout the project, Anguil provided onsite engineering assistance suggesting inexpensive changes, such as relocation of instrumentation or alternate piping plans to the equipment, which improved operations and maintenance activities. From an engineering standpoint, they were able to recommend improvements to customer specifications based on operational experience. These improvements included recommendations to upgrade materials of construction, alterations to process instrumentation, upgrading the size of the control panel touch screen to effectively display control parameters, and addition of important safety features. Furthermore, elimination of the redundant multiple control panels was accomplished by integration of logic into the Anguil supplied main system control panel. Lastly, because of site considerations, Anguil suggested substitution of the originally specified radio communications between the main control panel and remote injection well control panel with fiber optic connectivity. This ultimately resulted in a reduction of Anguil’s scope of supply, but greatly improved the system robustness and reliability.
As the project progressed, Anguil worked with the EPC engineering team on several customer-driven change orders. Most significantly, they worked with the EPC to specify and source additional flow meters for the injection well piping that were capable of accurate operation within the space constraints (limited straight run) dictated by the prefabricated concrete well vaults. Anguil managed ripple effect design changes including upgrading the effluent pump capacity, the motor control center and additional input/output cards for the local control panel – these changes were accomplished with no effect on the overall equipment delivery schedule.
In preparation of system start-up and shake down, Anguil on site personnel verified that all equipment was installed per manufacturer recommendations and was operating correctly. In several instances, they were able to identify equipment which had been installed improperly, delivered incorrectly or specified imprecisely. In most cases, these discrepancies were rectified quickly at no cost to the customer. As Anguil personnel accommodated continuing construction activities, PLC program operation was verified and altered as necessary to provide adequate system control. The final result was a turnkey system that met customer requirements for their commissioning schedule and operational characteristics so the project could start on time and on budget.
Balancing Low Fuel Consumption and High Destruction Efficiency at Remote Remediation Sites
Comments Off on Balancing Low Fuel Consumption and High Destruction Efficiency at Remote Remediation SitesTHE CHALLENGE
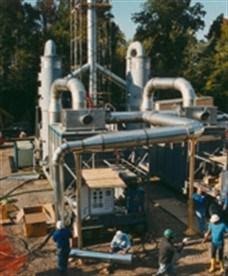
A large consulting and contracting firm owns and operates several ex-situ Thermal Desorption Units (TDUs) approved for use under the Resource Conservation and Recovery Act (RCRA); the Comprehensive Environmental Response, Compensation and Liability Act (CERCLA); as well as for use at private industrial remediation sites containing a wide variety of chlorinated and non-chlorinated contaminants up to concentrations of 3,000 ppmv. Being mobile, the TDUs can be deployed anywhere in the country and would be subject to varying local environmental regulations on hydrogen chloride (HCl) emissions produced from the thermal oxidation of halogenated compounds. Lastly, the operating cost of the full remediation solution directly affects the total project cost and ultimately the firm’s bottom line. To meet their technical and commercial project requirements, the customer was seeking an Air Pollution Control solution capable of handling a wide range of contaminants and mitigating HCl emissions all while being easily mobilized and possessing the lowest operational cost possible.
After a thorough technical evaluation and bid process, the customer selected a complete, mobile treatment package from Anguil Environmental Systems’ Wastewater Treatment team (FKA Global Technologies), containing a Chlorinated Catalytic Oxidizer (Chloro-Cat) and acid gas scrubber package. Anguil’s solution was selected due to our experience with over 30 such systems already installed to treat similar chlorinated streams from Soil Vapor Extraction sites as well as groundwater remediation sites utilizing air strippers.
THE SOLUTION
 A catalytic solution was selected largely due to the oxidizer’s compact body and ability to operate at lower combustion temperatures, making it mobile and cost effective to run as compared to a traditional Direct Fired Thermal Oxidizer. The lack of inexpensive natural gas feeds at many remediation sites dictates the use of propane for supplemental fuel and because direct thermal oxidation requires operating at temperatures between 1600°F – 2000°F considerable amounts of costly propane would be consumed over the course of the project. By contrast, each TDU could be expected to exhaust up to 5,000 SCFM of desorption air at temperatures between 400°F – 900°F which is at or near the minimum inlet catalyst temperature. Because the incoming process temp was already preheated by the TDU little supplemental fuel would be required by the Chloro-Cat. As with all Anguil chlorinated catalytic systems, a 316L stainless steel shell and tube heat exchanger would be installed in the 316L stainless steel reactor to further minimize propane consumption.
To mitigate HCl emissions, Anguil utilized a high temperature quench on the Choro-Cat exhaust followed by an acid gas scrubber constructed of Fiberglass Reinforced Plastic (FRP). HCl is removed from the air stream by interaction with either a recirculating caustic solution or using once through water. An induced draft FRP fan on the back end of the treatment package was provided to pull vapors through the system due to the high temperature, highly saturated exhaust from the TDU and the resultant HCl acid gasses.
As this was a soil heating application, utilization of a high-temperature baghouse dust collector on the TDU skid removed concerns associated with dust or dirt plugging of the monolithic catalyst cells.
Anguil was able to package the entire system onto a 50′ drop deck trailer. In addition to the Chloro-Cat and scrubber, the trailer included a Liquid Propane Vaporizer and a storage area for equipment transport.
THE RESULT
Anguil’s experience proved invaluable in designing and implementing the proper solution for this application. The chlorinated catalytic system was designed to provide 99% destruction efficiency at operating temperatures of 500°F – 850°F to reduce auxiliary fuel usage and meet the customers’ needs for performance and low OPEX. Safety systems were installed to ensure no HCl condensation to minimize equipment corrosion to protect the customer’s investment, and with the modular trailer mounted solution, eased the customer’s ability to deploy to multiple sites. The most recent compliance testing of this turnkey package demonstrated over 99% destruction of all compounds.