




Plastic Components Painting
Comments Off on Plastic Components PaintingThe Challenge
A plastic injection molding company in Wisconsin is known as a world-class leader in the industry for their secondary decorating and assembly capabilities. One of their eleven facilities not only perform plastic injection molding but also provides the organization with decorating capabilities such as painting, laser etching, laser marking, pad printing and assembly of automotive, telecommunication and consumer products.
Over the years and through the 1990’s the operation ran successfully with a minor source air pollution control operation permit. This permit consists of very specific requirements to meet the Environmental Protection Agencies (EPA) LACT (Latest Available Control Technology) regulation. These included restricted limits on volatile organic compounds (VOC) per gallon of paint, catalyst, thinner and cleaning solvent as purchased. This limited the types of paints and colors they could offer customers but given the customer needs and production volume at the time, this was a manageable situation.
As the business grew, requests by customers for more exotic forms of paint and colors increased and they realized the need to increase their paint capabilities to compete. In December 2000 they applied for two new permits with The Department of Natural Resources (DNR), one for an air pollution construction permit to install a new state of the art robotic paint line system and the other for the ability to paint small metal parts. This permit modification changed the facility from a minor source of less than 100 tons per year of volatile organic compound emissions to a major source with the potential to emit over 225 total tons.
With the new permit, they not only had to meet the LACT requirements for the painting of plastic parts but now also needed to meet the MACT (Maximum Achievable Control Technology) requirements for the painting of small metal parts. The MACT requirements added a higher level of restrictions to VOC’s per gallon of paint as applied to metal parts. These restrictions were applicable and once again manageable.
Although the new permit allowed them to meet additional painting volume capacity requirements, they observed continued demand by their customers for paints that could not be used under the air permit. Additionally, with the acceptance into the ISO 14001:1996 standards, they realized the need to significantly reduce their VOC emissions.
The Solution
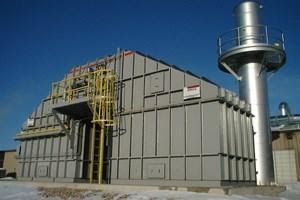
The only way to meet the customer demands and reduce emissions was to evaluate various forms of pollution control technologies. Anguil’s group of engineering experts convened to explore the various control technologies currently available on the market. Consideration was given to equipment/concepts such as:
- Catalytic Oxidizers
- Thermal Oxidizers
- Regenerative Thermal/Catalytic Oxidizers
- Emissions Concentrator Coupled with a Regenerative Thermal Oxidizer
- Microwave VOC Reduction Technologies
- Biofilter VOC Reduction Technologies
The company began to work very closely with the sales and engineering team at Anguil and the DNR to establish the best available control technologies to meet the pollution control requirements. With some simple calculations, Anguil was able to show how a Regenerative Thermal Oxidizer (RTO) would be the most cost-effective control technology for their current and future process demands.
The Result
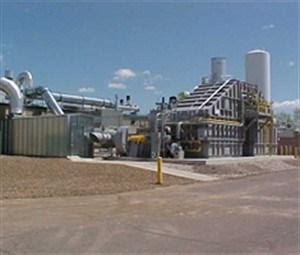
After thoroughly evaluating several suppliers the company decided to go back to the Department of Natural Resources and request a new air pollution control construction permit to install a Anguil Model 400 / 40,000 SCFM (62,800 NM3/hr) Regenerative Thermal Oxidizer (RTO) for their existing paint operations.
The oxidizer would achieve destruction through the process of high temperature thermal oxidation, converting the VOCs to carbon dioxide and water vapor while reusing released thermal energy to reduce operating costs. Process gases with VOC contaminants enter the oxidizer through an inlet manifold. Dual disk poppet valves direct this gas into energy recovery chambers where the process gas is progressively preheated by the ceramic media beds as they move toward the combustion chamber.
The VOCs are oxidized in the combustion chamber, releasing thermal energy in the structured ceramic media beds that are in the outlet flow direction from the combustion chamber. These outlet beds are heated, and the gas is cooled so that the outlet gas temperature is only slightly higher than the process inlet temperature. Fast acting vertical poppet valves alternate the airflow direction into the ceramic beds to maximize energy recovery within the oxidizer. The VOC oxidation and high energy recovery within these oxidizers reduces the auxiliary fuel requirement and saves operating cost. For example, at 95% thermal energy recovery, the outlet temperature may be only 70`F (40`C) higher than the inlet process gas temperature with an RTO. The oxidizer can reach self-sustaining operation with no auxiliary fuel usage at low VOC concentrations.
Programmable Logic Controllers (PLCs) control the automatic operation of the oxidizer from startup to shut down, so minimal operator interface is required. These controls also provide for remote telemetry to enable the system’s operation to be viewed and altered via remote connections to reduce maintenance costs.
Later that fall the permit was accepted by the DNR for an air pollution control construction permit to install an Anguil Regenerative Thermal Oxidizer. Anguil Environmental Systems was able to complete the design, fabrication, delivery, installation and startup of the RTO so it could go on line early the next year.
After startup of the new RTO, a stack test measured 99% destruction rate efficiency for volatile organic compound (VOC) emissions at 100% capture. This equated to a net reduction of 58 tons of VOC emissions in the first 6 months of operation.
The benefits of installing the RTO included the ability to offer customers a large variety of paints and colors to meet their more unique paint finish requests. Also, the RTO allowed the manufacturer to use previously restricted thinners and paints to better process their products with fewer rejects. This allowed the business to grow and succeed in an increasingly competitive environment and meet the new demands from customers while significantly reducing the amount of volatile organic compounds released into the environment.
Turnkey VOC Control for High-Volume Paint Spray Operations
Comments Off on Turnkey VOC Control for High-Volume Paint Spray Operations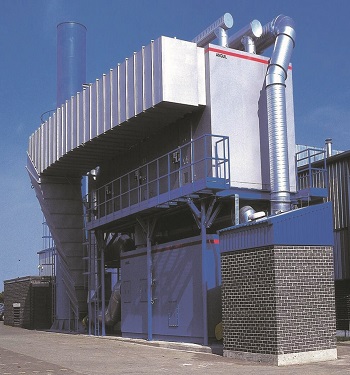
THE CHALLENGE
A major automotive component supplier needed to control the emissions from its paint spray process. The plant emissions had characteristics common to many paint spray plants: high air flow, low volatile organic compound (VOC) concentration and particulate. The company needed an emission control solution that had low operating costs and that could also fit in their limited space. System reliability was also a major design consideration; since the company is a synchronized delivery partner to the automobile industry, plant downtime or process delays result in expensive fines.
THE SOLUTION
After an extensive technical evaluation of the proposed technologies and equipment manufacturers, the customer chose Anguil Environmental Systems to provide a turnkey solution for the VOC and particulate emissions. Anguil recommended an Emissions Concentrator coupled with a Thermal Oxidizer System to effectively process the 120,000 SCFM (190,000 Nm3/hr) of plant exhaust.
THE RESULT
The cost of an emission control system is driven largely by the volume of air that must be treated, making paint spray operations expensive due to their high process exhaust requirements and relatively low VOC concentration. Anguil’s Emission Concentrator addresses this by reducing the air volume sent to the oxidizer by a factor of 15. In this application, the 120,000 SCFM paint booth airstream is absorbed by the Zeolite Concentrator Wheel. The VOCs are then desorbed in a separate 8,000 SCFM stream with elevated VOC levels ~4500 ppmv which is sent to a Regenerative Thermal Oxidizer (RTO). This dramatic decrease in exhaust flow reduces the size of the oxidizer needed as well as decreases the operating cost.
Anguil custom engineered this technology based on the key requirements. Reliability was critical for this Tier One automotive supplier, where downtime can result in fines up to $30,000 a minute; Anguil incorporated advanced Programmable Logic Controls (PLC), built-in safety features, and seamless integration into the existing process. Tight space constraints and local noise limits drove the development of a vertical system design that reduced the footprint by 70% compared to competing RTO vendors and the inclusion of sound-attenuation features to meet local requirements. To manage heavy paint particulates often found in paint spray applications, Anguil included a high-efficiency filtration system with simple low-cost filter replacements.
Anguil provided a full turnkey installation of the system that meets the facility’s space and noise limitations, exceeds regulatory requirements, and provides long-term cost savings through the highly efficient air volume reduction approach.
Streamlining the Stream: How Innovative Capture Design Slashed Exhaust Volumes and Compliance Costs
Comments Off on Streamlining the Stream: How Innovative Capture Design Slashed Exhaust Volumes and Compliance Costs THE CHALLENGE
 THE CHALLENGE
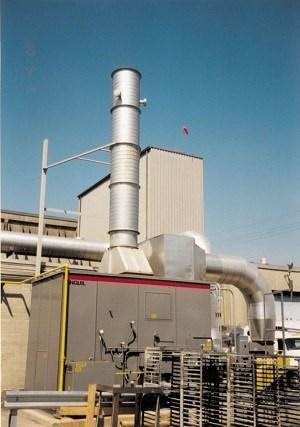
A company involved in the automotive aftermarket had a paint batch mixing and filling operation that used primers and fillers. They needed to install equipment to handle the volatile organic compounds (VOCs) emitted during their processes. An independent consultant determined the total exhaust volume from the facility was 28,000 SCFM (44,940 Nm³/hr) of air and contained relatively low concentrations of solvent vapors. This combination of high exhaust volume and low vapor concentration posed an operating cost problem. Powder added into the batch mixers generated dust, posing potential hazards to the operators and OSHA (Occupational Safety and Health Administration) violations added an additional challenge.
THE SOLUTION
Anguil analyzed the data, operation, and needs of the customer. A major consideration was on the composition of the solvents and high air volume. Of the solvents used, a small portion was methylene chloride. Chlorinated compounds are a potential poison to most catalytic systems and the company’s consultant recommended a thermal incinerator. Anguil recognized that a less expensive alternative to a thermal unit would be a Chlorinated Catalytic Oxidizer, which is specially designed to process chlorinated compounds. However, Anguil recommended an evaluation of alternate compounds to replace the chlorinated organics. Upon investigation, the company chemist determined all the chlorinated compounds could be replaced with regular organic solvents. Thus, eliminating the need for a Chlorinated Catalytic Oxidizer.
The high air volume was further analyzed. One of Anguil’s strengths is knowledge in capture hooding and air flow reduction techniques. The 28,000 SCFM (44,159 Nm³/hr) exhaust was originally recommended on the assumption that all 13 batch mixing devices could be at their peak mixing and vapor loading capacity simultaneously. Interviewing the facility manager, it was determined that all 13 mixers were never loaded simultaneously.
After a comparison of various proposals, Anguil Environmental Systems was contracted. Anguil developed and designed an air reduction system after mapping the VOCs with a portable Flame Ionizing Detector (FID). This research allowed engineers to determine the area of high VOC concentration and design an innovative capture system that drastically reduced the amount of air treated.
THE RESULT
The company was using floor sweeps as part of their capture system, but they were up to ten feet away from the mixing devices. Additionally, the mixing container covers were poor fitting and extremely heavy. Anguil’s solution included replacing the floor sweeps and tank covers with a close capture hooding system. A series of aluminum custom fabricated covers with integrated flexible duct connectors to draw the vapors and dust directly from the mixers were created. The added benefit of the close capture hooding was a decrease in air volume necessary to capture the vapors from the VOC source.
Anguil determined the VOCs from the mixing room could be adequately captured with 9,000 SCFM (14,194 Nm³/hr) of air and that plans for expansion would not take the exhaust air volume above 12,000 SCFM (18,925 Nm³/hr). Rather than focusing on costly outside air to replace the 9,000 SCFM (14,194 Nm³/hr), Anguil supplied close capture pick-up hoods in the mixing room adjacent to the room containing the fill devices. This air was then transferred into the adjacent mixing room, creating makeup air. The VOC concentration of this air was well below the Threshold Limit Values (TLVs), but the state regulatory authorities determined these VOCs were at an unacceptable limit and should be destroyed. The air supply was introduced on the far side of the mixing room which helped sweep the vapors across the 120 by 60-foot room toward the pick-up points.
Outside of the building, a 12,000 SCFM (19,260 Nm³/hr) catalytic oxidizer was installed on a concrete pad. Prior to entering the catalytic oxidizer, the airstream was fed through a two-chamber dust collector to prevent the particulates from masking the catalyst or blocking the oxidizer’s plate type heat exchanger. A precious metal platinum catalyst was chosen to destroy the hexane and toluene organics. Catalyst was provided to process 9,000 SCFM (14,194 Nm³/hr) and as the facility capacity increased, more catalyst could be added. Due to the well-designed air reduction strategy, Anguil saved the customer tens of thousands of dollars on their pollution control system while achieving compliance.
Natural Gas Production
Comments Off on Natural Gas Production The Challenge
 The Challenge
The largest U.S.-based independent oil and gas producer and one of the largest independent processors of natural gas and natural gas liquids in North America was in search of new technologies to maintain the pollution control efficiency at their natural gas treatment facility.
In typical gas plants, the wellhead natural gas needs to be treated to remove water, CO2, any sulfur compounds and heavy hydrocarbons before it is sent to the pipeline. The acid gases formed by CO2 and H2S are normally removed by amine adsorption. The amine must then be stripped of these acid gases in order to be reused. The amine stripper off gas (tail gas) needs to be treated before discharge to atmosphere to remove residual hydrocarbons and meet EPA regulations.
The Solution
Gas and oil plants have historically used direct-fired thermal oxidizers with no heat recovery for tail gas treatment. The existing thermal oxidizer at this facility was using a considerable amount of auxiliary fuel to maintain temperatures of 1,500°F, ensuring all the organics were combusted but costing them a significant amount of money in operating costs. Dedicated to finding a less expensive means of regulatory compliance, the oil and gas producer challenged several air pollution control manufacturers to provide a system that was not only effective, but also energy efficient.
When Anguil was approached to address the air pollution control needs at this facility, careful measures were taken to assure the proper equipment selection.
The Result
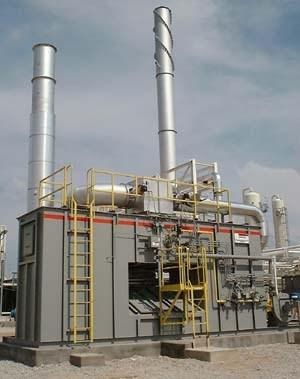
After much consideration, Anguil offered their Model 75 (7,500 SCFM, 12,037.5 Nm3/hr) Regenerative Thermal Oxidizer (RTO) with heat recovery for efficient and effective operation. Anguil was selected because of their unique approach toward air pollution control and energy conservation.
With the Anguil two-bed RTO, the contaminated process gas is pre-heated as it passes through beds of ceramic media located in the energy recovery chambers. The process gas moves from the pre-heat chamber toward the combustion chamber, where the Volatile Organic Compounds (VOCs) are oxidized, releasing energy into the second energy recovery chamber before going to atmosphere. A diverter valve switches the process gas direction so both energy recovery beds are fully utilized, thereby reducing any auxiliary fuel requirement. This system is designed for heat recovery of 85% and is self-sustaining, requiring little auxiliary fuel use. This energy-efficient design offers significantly lower operating costs in comparison to other emission treatment methods.
The RTO is designed to prevent corrosion by the acid gases and to handle the high organic loading with low oxygen levels. The gas at this facility is “sweet” and does not contain any H2S but precautions were taken to prevent carbonic acid attack due to the CO2. In addition, Anguil provided a Class 1, Division 2, Group D control package. Heated, fresh air was also introduced into the system, providing supplemental oxygen without condensing moisture in the process stream. Anguil’s application specific engineering was an important factor in the success of this project.
The Anguil RTO is achieving 99% DRE (Destruction Rate Efficiency) and is saving the customer more than $500,000 per year in natural gas costs. Anguil’s equipment, detailed system design, installation and startup has exceeded the customer’s expectations of efficiency and affordability.
Amine Tail Gas Treatment
Comments Off on Amine Tail Gas TreatmentTHE CHALLENGE
With the discovery of new shale formations throughout the world, and the development of new drilling technologies, natural gas production has increased. The rise in production has prompted government agencies to initiate tighter air-pollution control regulations on processing operations. Sustaining environmental regulations is not typically a profit-generating endeavor. As a result, saving money while meeting regulations should be every midstream company’s priority.
Much like other industries, oil and gas producers are often required by the Environmental Protection Agency (EPA) to obtain a Title V permit. Title V’s objective is to prevent untreated air pollutants from entering the atmosphere. In addition to their harmful effects on the environment, these pollutants, known as volatile organic compounds (VOCs) and hazardous air pollutants (HAPs) have been linked to respiratory ailments, heart conditions, birth defects, nervous system damage, and cancer in humans.
Under the Clean Air Act, most companies with the potential to release more than 10 tons of a single VOC or HAP during a one-year period, or 25 tons of multiple compounds, must install either a pollution-control device. Many of the pollution control devices currently used to abate these emissions also emit significant amounts of carbon dioxide (CO2) and nitrous oxides (NOx). With mandatory greenhouse gas (GHG) reporting on the horizon, processors could soon be paying for the carbon emissions generated by some of these pollution control systems, adding to the capital and operating costs associated with regulatory compliance.
Several production techniques and processes used by midstream companies are, or soon will be, regulated as emission sources. From stationary combustion engines to amine systems, the industry is facing strict legislation.
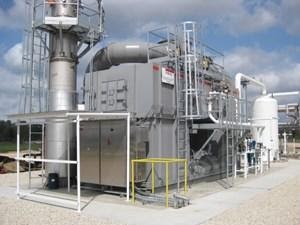
The midstream division of a large, multinational energy corporation was operating several amine systems around the country with tail-gas treatment. A thermal oxidizer (TO) at one of these facilities had numerous operational problems and extremely high operating costs.
Amine tail-gas treatment is one area of great legislative concern in the industry. Amine systems are a very common and critical component used by natural gas-processing facilities to remove acid gases, carbon dioxide (CO2), and hydrogen sulfide (H2S). This is accomplished by running the gas through a column with amine liquid flowing in the opposite direction, stripping acids from natural gas and absorbing them into the liquid. The natural gas is then sent for processing while the amine is sent to be regenerated. The regeneration process removes the acid gases from the amine solution, allowing it to be reused, but the process creates tail gas. This tail gas, and the means for treating it, offer the latest opportunity for the implementation of new technologies and increased profits.
Thermal and catalytic oxidizers are technologies commonly used on a wide variety of applications where VOC, HAP, and odor abatement is required. They destroy harmful emissions through the process of high-temperature combustion. Midstream companies have historically used flares, vapor combustors, direct-fired thermal oxidizers (DFTOs), or recuperative systems for emission destruction. Applications where these devices are applied range from amine tail-gas treatment, nitrogen rejection units, and liquefied natural gas (LNG) processes. The temperature in these systems is maintained somewhere between 1,400°F – 1,800°F (760°C – 982.2°C) so that hydrocarbons are converted to CO2 and water vapor, while the H2S is converted to sulfur dioxides (SO2 and SO3).
When designed properly these older technologies are dependable, but their effectiveness sparks heated debate. In the case of flares, water is often injected into the device to reduce visible black smoke. This drastically reduces the destruction efficiency — and the EPA is taking note. Large amounts of fossil fuels are required to bring the air toxins up to proper destruction temperature. Rather than use the heat generated from combustion to preheat incoming pollutants, the energy is simply released into the atmosphere, along with GHGs.
A proven fuel-efficient abatement technology called the regenerative thermal oxidizer (RTO) is now being applied to tail-gas treatment where it was once thought impossible. What differentiates it from other technologies is its ability to use the proper mix of temperature, residence time, turbulence, and oxygen to convert pollutants into carbon dioxide and water vapor. The system reuses the thermal energy generated to further reduce operating costs. In some cases, emission destruction can occur without any additional natural gas or other supplemental fuel.
VOC- and HAP-laden process gas is routed into the inlet manifold of the oxidizer, flow control, or poppet valves. These valves then direct this gas along with fresh air for combustion into energy-recovery chambers where it is preheated. The process gas and contaminants are progressively heated in the ceramic media beds as they move toward the combustion chamber.
Once oxidized in the combustion chamber, the purified acid gas releases thermal energy as it passes through the media bed in the outlet flow direction. The outlet bed is heated, and the gas is cooled so that the outlet gas temperature is only slightly higher than the process inlet temperature. Poppet valves alternate the airflow direction into the media beds to maximize energy recovery within the oxidizer.
Thermal energy recovery (TER) within an RTO can reach 97%, which in some cases eliminates the auxiliary fuel requirement. Some gas plants have reported over $500,000 in operating cost savings annually. With destruction capability over 99%, the RTO is an efficient alternative for this application. However, careful consideration must be given to the design and materials of construction to avoid corrosion, equipment failures, non-compliance, and safety issues.
THE SOLUTION
The company asked Anguil Environmental Systems to evaluate replacement options. The process data provided showed a tail-gas flow rate of about 15,000 lbs/hr or about 2,500 SCFM (4012.5 Nm3/hr). After evaluating numerous oxidizer technologies, including TOs and thermal recuperative oxidizers, Anguil determined that the best solution would be an RTO. Having designed oxidizers for similar corrosive applications, the engineers at Anguil recommended the RTO be built with special materials and design considerations to combat the presence of both carbonic and sulfuric acid.
Carbonic acid is caused by high CO2 levels combined with a saturated process stream. Sulfuric acid is created when H2S is oxidized and the resulting SO3 combines with water vapor present in the RTO exhaust gas. The amine process exhaust at this midstream operation was inert, or lacking oxygen; therefore, fresh air was required for oxidation. Heat released from combustion of these hydrocarbons can be very high, so fresh air is also added to keep the system from running over temperature. To eliminate condensation of water vapor of the tail gas inside the RTO, this ambient air is preheated to protect metal surfaces from inorganic acids condensing.
THE RESULT
A system utilizing excess heat from the combustion chamber to provide the necessary heat was deployed on this system, further reducing operating costs. The preheat component eliminates the need for additional equipment and further minimizes auxiliary fuel consumption. The next step in the corrosion-protection strategy is to implement various stainless-steel alloys on critical components and a corrosion-resistant coating on the inside of the energy-recovery and combustion chambers.
The critical components are chosen based on their function within the RTO. These components see exhaust temperatures of up to 600°F (315°C), above the limit of corrosion-resistant coatings. The energy recovery and combustion chambers are internally insulated with soft ceramic refractory insulation, limiting the shell temperature to 200°F (93°C), well below the safe limit of the coating. With the combination of extremely high TER, and the tail-gas calorific value of 6 Btu/SCF, this RTO requires no auxiliary fuel to achieve 99% destruction efficiency.
Protecting the environment, meeting regulations, and saving money are not mutually exclusive. Re-evaluating, and upgrading abatement technology should be a priority for every industrial manufacturer.
Organic Particulate Filtration
Comments Off on Organic Particulate Filtration The Challenge
 The Challenge
A food products company that mixes various types of waxes and other components to make the base for chewing gums was faced with the issue of cleaning up a slightly odorous, visible emission being exhausted from two of their process lines. The components of the emission were hot particles of chewing gum and some volatile organic compounds (VOC’s). The particles would quickly clog a conventional filter system or electrostatic precipitator, neither of which could control the odor off the process line. In addition to the emission problem, the condensation of the exhaust stream was damaging the roof of the facility.
The Solution
After thorough technical evaluation, the Self-Cleaning Ceramic Filter (SCCF) was recommended as the ideal solution for processing the exhaust and Anguil Environmental Systems was selected to solve the visual, odor and VOC problem.
The Result
In order to demonstrate to the client that this was a viable solution, Anguil utilized their portable self-cleaning ceramic filter test unit before any purchase decisions were made. During the test, the process lines were run through the ceramic filter in two modes, hot and cold.
First, the system was run in the hot mode with a gas burner firing continuously at 400º-500ºF heating up the process air. The once visible plume disappeared as it passed through the ceramic filter and catalyst module. Second, the ceramic filter was used without heat, and again, the visible plume disappeared as it passed through the ceramic filter and catalyst module. Twenty-four hours of production were run across the ceramic filter without heat and the visible emission was acceptable from a customer and environmental regulation standpoint. However, when utilizing a cold process stream, particulate matter accumulated on the ceramic filter which had to be periodically cleaned by firing the burner. When the cleaning cycle began after the two shifts, a dense white plume was emitted for 90 seconds while the filter element was burned clean. The customer, a food products company, felt that this emission level was not acceptable so they decided the continuous hot running ceramic filter would better fit their needs. It should be noted that for certain operations with visible emissions, the pulse cleaning mode may be acceptable. Many local authorities allow companies to discharge up to five minutes per hour without control.
After the customer determined that the ceramic filter would solve their problems, Anguil proceeded to manufacture and install a 1,000 SCFM (1,577 Nm3/Hr) ceramic filter unit. The unit was used to process the exhaust from two process lines. One of the more significant benefits to the company was Anguil’s ability to reduce the air volume from the processes. Initially, the two gum-based mixers each had a 3,000 SCFM (4,731 Nm3/Hr) high volume, low static pressure fan that was exhausting to atmosphere. Tight covers on the mixers minimized the escape of odor into the mixing room. With the close capture hoods it was possible to reduce the air volume from 6,000 SCFM (9,462 Nm3/Hr) exhaust to 1,000 SCFM (1,577 Nm3/Hr) exhaust from the two process lines. The net air volume reduction of 82% reduced both the capital cost and the operating cost of the system.
In order to guarantee continuous production in the event of a burner failure, Anguil installed a bypass equipped with conventional roughing filters. The exhaust fan was equipped with an inlet vane control to vary the air volume if only one process line was being used. The control panel was outfitted with a user-friendly PLC first out detection system. The entire ceramic filter system was mounted in a light-weight enclosure to allow for roof mounting without significant structural modifications to the building. Growth capacity was accommodated in the gas burner and the fan section, allowing for the addition of future operations. Anguil’s system engineering provided their client with a solution to their compliance needs at reduced air volume and reduced cost.
Meat Processing Odor Control
Comments Off on Meat Processing Odor Control The Challenge
 The Challenge
For its first two years of production, a food manufacturer based in South Wales, England, focused its production on potatoes. Neighborhood residents voiced no complaints about odors during this time period. However, as new production lines (including barbequed meats and curried chicken) were added, the complaints began, and it became clear that odor abatement equipment was needed to resolve the issue.
Onsite meetings were held to discuss the issue, concerned citizens and the local environmental health officer attended to discuss the best way to handle the situation. The company employs a large percentage of the local residents, and was concerned about maintaining good community relationships, while at the same time it was in need of a building expansion to introduce a new line of curried chicken products. Planning approval became contingent upon the installation of an odor abatement system to control the new and existing odors.
The two-year old factory had been designed to incorporate emission control equipment, and management was committed to installing the most effective technology available. After a thorough technical evaluation, Anguil Environmental Systems, Inc. was selected and contracted to address the odor emission problem and satisfy the building expansion requirements.
The Solution
Although several odor control technologies were discussed — including masking sprays, wet scrubbing, bio-filtration, carbon absorption and catalytic and thermal oxidation — the Regenerative Thermal Oxidizer (RTO) was the only technology that could guarantee the elimination of 99% of the odorous compounds.
Since future production may produce different odors, it was necessary that the installed technology have the ability to treat a wide range of odorous compounds to a high level of removal/destruction – guaranteed. Although, the guarantee of nearly complete elimination of the odors was the primary concern, capital and running costs were also of utmost importance. The RTO was selected due to its low operating costs and the fact that no waste is produced as a byproduct of its functioning.
The Result
 The Result
Following the installation of the RTO, the results were dramatic, and as promised nearly all of the odors have been eliminated. Due to its well-designed odor control strategy, Anguil resolved the odor emission problem, thereby resolving potential community relations/environmental issues, and meeting its requirements for obtaining planning approval for future expansions.
Reducing Dependence on Natural Gas in the Bean Roasting Industry
Comments Off on Reducing Dependence on Natural Gas in the Bean Roasting IndustryTHE CHALLENGE
Emissions and odors from the bean roasting process have traditionally been treated with an afterburner. This process simply burns the roaster exhaust with natural gas or other fuel types. While this is an effective means of air pollution control, it is not energy or cost efficient.
Recognizing the challenges, Anguil set out to build a more energy-efficient, cost-effective means of handling emissions in the bean roasting industry. Ultimately, Anguil established a system that not only accounts for the unique needs of the application but also achieves environmental compliance at a fraction of the operating cost.
After purchasing a new roaster, a nationally known chocolate roaster company knew their exhaust process needed an upgrade for the increased facility output. Rising fuel costs and sustainability concerns prompted this company to find a more energy-efficient, cost-effective means of emission destruction. Anguil recommended an 8,000 SCFM (12,840 Nm³/hr) RTO to handle the new roaster, nip grinder, and alkalizer at this facility.
THE SOLUTION
With a two-bed regenerative thermal oxidizer (RTO), contaminated process gas is preheated as it passes through beds of ceramic media located in the energy recovery chambers. The process gas moves from the pre-heated chamber toward the combustion chamber, where the volatile organic compounds (VOC) are oxidized, releasing energy into the second energy recovery chamber before discharging to the atmosphere. A diverter valve switches the process gas direction so both energy recovery beds are fully utilized, providing 95% thermal efficiency thereby reducing auxiliary fuel requirements. Under normal operating conditions the unit is self-sustaining, requiring no additional fuel to achieve destruction.
For every 2,500 SCFM (4,012 Nm³/hr) of process airflow increase, the afterburner requires 18 times more natural gas than the RTO. For this application the RTO technology uses, on average, 12 times less natural gas compared to a traditional afterburner. At $5/MMbtu for natural gas, that could result in over $500,000 in savings for a 24/7 operation utilizing a four-bag roasting machine. This energy-efficient design offers significantly lower operating costs in comparison to other treatment methods commonly used in bean roasting facilities.
THE RESULT
Water vapor was a concern during the design phase of this project, so accommodations were taken to handle the high moisture airstream from the roaster. Water is also added for flavor and sterilization purposes. If precautions are not taken, it could cause system components to seize during freezing weather, accelerate corrosion of carbon steel parts resulting in oxidizer shutdowns during high production times. Anguil engineers recommended a knockout drum with removal pump just upstream of the RTO. Modifications were also made to the fresh air damper to introduce less water vapor and portions of the ductwork were insulated to prevent freezing.
Special consideration was given to the RTO ceramic media to account for any particulate in the airstream, ensuring proper operation. The oxidizer also has a bake-out feature which works much like the self-cleaning feature on an oven. Organic particulates are regularly burned out during a high temperature cycle, which ensures the media does not plug, reduces pressure drops, and lowers electrical consumption.
In addition to the emission and odor control equipment, Anguil provided a 7,000 SCFM (11,235 Nm³/hr) plate heat exchanger and corresponding duct work. This sends approximately 1.5 MMbtu/hr of waste heat from the RTO exhaust stack to a make-up air unit on the roof. This adaptation saved the company over $80,000 a year in heating costs during winter months. On similar applications, Anguil has returned waste heat back to the roasters, which further reduces natural gas consumption and operating costs.
The company was so pleased with the solution Anguil provided; they have purchased two similar systems for their other facilities. The updated systems have resulted in environmental compliance, and lower operating costs for the bean roasting company at all three plants.
Stainless Steel RTOs for Ethanol Emissions and Odors
Comments Off on Stainless Steel RTOs for Ethanol Emissions and Odors The Challenge
 The Challenge
A 42 million gallon expansion at an ethanol production plant in the Midwest was certain to put the dry mill out of compliance for emissions such as Hazardous Air Pollutants (HAPs), Volatile Organic Compounds (VOCs), carbon monoxide (CO), nitrogen oxides (NOx), and particulate matter (PM). In general, ethanol production facilities in the United States are permitted to operate under a ‘minor source’ status as long as the total tonnage of key pollutants are below the 100 tons (named sources) or 250 tons (non-named sources) per year limit. However operating restrictions, penalties and fines, as well as community pressures are forcing many plants to strive for the lowest possible emission levels, enabling future capacity expansions.
The Solution
Anguil was awarded a multi-million dollar contract to assist the ethanol plant in meeting Environmental Protection Agency (EPA) regulatory requirements.
The Result
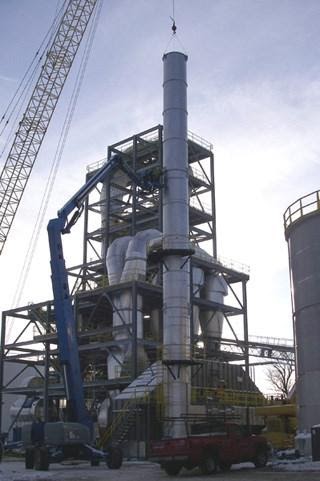
Known for their low operating cost and high destruction rate efficiency, the Anguil Regenerative Thermal Oxidizer (RTO) was selected as the best available control technology for the application. The pollution control device consists of two side-by-side Anguil RTOs handling a process volumetric flow of 120,000 SCFM (Standard Cubic Feet per Minute) (192,600 Nm3/hr). The system will achieve greater than 99% destruction rate efficiency for air pollutants and odorous emissions with 95% thermal energy recovery, ensuring low fuel usage. Portions of the equipment are constructed of 304-stainless steel to protect against corrosion from the ethanol process stream. The project scope consists of equipment design, manufacturing, installation supervision, process integration and start-up.
While several options and suppliers were considered, Anguil was awarded the contract after the Midwest producer evaluated system reliability, capital costs, destruction rate efficiency and operating cost estimates.
Keeping Ethanol Production Green
Comments Off on Keeping Ethanol Production Green The Challenge
 The Challenge
In an effort to reduce the world’s dependence on fossil fuels, there has been a major push towards alternatives. Ethanol has been at the forefront of this movement because it reduces greenhouse gas emissions from automobiles and its production has a positive net energy balance. The homegrown fuel also reduces the need for imported oil from sometimes unfriendly and unreliable supplier nations.
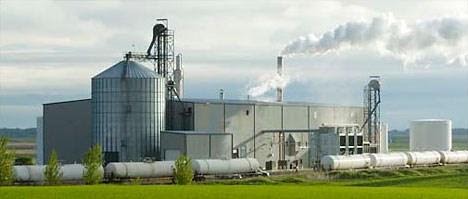
Ethanol is produced by fermenting and distilling starch, creating a 200-proof alcohol suitable for combustion in a vehicle. When processing corn, only 70 percent of the kernel is made into ethanol; the remaining fats, proteins, fiber, oils and minerals are referred to as distiller’s grain (DG). If a production plant is not very proximate to dairy operations or other significant livestock feeding needs, it will have to dry the DG in order to prevent spoilage during transport to more distant regional markets. Operating restrictions, penalties and fines, as well as community pressures, are forcing many plants to strive for the lowest possible emission levels from their dryers, enabling future capacity expansions.
Since air permits are granted on a facility-wide basis, when developing, designing and permitting ethanol production facilities, selecting the most appropriate process equipment as well as air pollution control equipment is critical. Some unique DG dryer designs are steam-heated or compressed air-based, but the vast majority of installed dryers are heated with natural gas. Regardless of the dryer type, volatile organic compounds (VOCs), odors and aerosols are emitted from the drying activity. By far the most commonly installed technology for this critical emissions source is some form of efficient thermal oxidation. Most of the major ethanol design firms incorporate thermal oxidation of this exhaust stream into their plant designs, and most state air permitting agencies require it.
The Solution
 The Solution
Process configurations & air permit implications
Selecting a dryer technology and its corresponding pollution control equipment often is the underlying decision for determining air permitting major source status. Prevention of significant deterioration (PSD) thresholds are now 250 tons per year (tpy) per pollutant facility-wide, since the EPA changed its interpretation of PSD rules for ethanol plants, in 72 FR 24060, on May 1, 2007.
In some non-corn-belt areas of the country where ethanol plants are now being proposed, such as those in ozone non-attainment areas or transport regions, major source thresholds are as low as 50 or even 25 tpy of VOCs to trigger non-attainment New Source Review (NNSR) permitting. When combustion emissions from boilers, emergency generators, fire water pump engines and load-out flares are added to those from the dryer and thermal oxidizer, one can envision why these decisions are critical.
NNSR permitting involves determining and installing the lowest achievable emissions rate (LAER), control technology, obtaining emissions offsets, and analysis of alternatives for the entire development project. PSD permitting involves dispersion modeling, best-available control technology (BACT) determination and commitment, and other impact analyses. Both NNSR and PSD permitting involve additional expense and longer permitting timelines, neither of which finds fondness with ethanol developers. Efficient, properly tuned thermal oxidizers are generally considered to meet BACT and LAER requirements, but there is surprisingly little history in the EPA’s RACT/BACT/LAER Clearinghouse database[1], since most ethanol developers to date have sought to avoid NNSR and PSD permitting by maintaining emissions below the threshold levels.
Abatement equipment selection
Some ethanol facilities in the upper Midwest were originally constructed without thermal oxidizers. However, odor complaints and EPA consent orders forced the installation of oxidizers, and hence some form of thermal oxidation is now a part of any new ethanol plant design involving a dryer. Certain plants with solid fuel boilers (often major sources) may vent the dryer exhaust into the boiler for thermal destruction. Others may recover some energy from direct-fired thermal oxidizers by generating steam.
In general, the following two technology solutions have been considered preferred for the ethanol plant DG dryer emission control:
Regenerative thermal oxidizer (RTO):
- Destruction Efficiencies of 98 to 99% for VOCs, hazardous air pollutants (HAPs) and CO
- Designed to handle a wet air stream with some particulate.
- Pre-filters available for higher levels of particulate.
- Thermal energy recovery of 95 percent insures low fuel usage, and low NOX production.
- Fuel injection system further lowers NOX.
Direct-fired thermal oxidizer (DFTO) with waste heat boiler:
- Designed to oxidize 99+ percent of VOCs, HAPS, CO and organic particulate without obstructions, eliminates the potential for plugging.
- Generates steam for use in the process.
- Can reduce overall capital cost of plant and air emissions.
- Optional turbine produces power for driving electric motors or for distribution within the plant.
The Result
A natural gas RTO may have the highest efficiency, the lowest emissions and a lower total installation cost versus other options. A natural gas RTO may allow a larger capacity plant to be constructed (greater than 100 MGY) while remaining a minor source, but most other options will trigger major source permitting. Trade-offs are between capital expenditures and operating expenses, as well as a shorter timeline to construction, versus potential future competitive advantages. A good natural gas supply deal is a must, with some portion of the net input reserved for hedging on the spot market.
An ethanol developer’s speed-to-market, permitting timeline and expenses, material logistics, feedstock, energy source, and selected co-products all relate to the dryer type and air pollution control technology decisions.
Several other parameters need to be considered to evaluate the selection and design of a fully integrated air abatement system, including regulatory requirements and emission characteristics for VOCs, NOX, CO and HAPs. Other parameters include the following process characteristics:
- New or existing plant
- Airflow requiring treatment
- Steam requirements and cost to produce
- Power availability and cost to distribute
Environmental impact
According to the Department of Energy’s Argonne National Laboratory, ethanol-blended fuels reduced CO2-equivalent greenhouse gas emissions by 7.8 million tons in 2005, which had the equivalent effect of removing the annual greenhouse gas emissions of over 1 million automobiles from the road. Many agree that ethanol is a cleaner-burning fuel than gasoline. With state-of-the-art control technology in place at ethanol plants, it can be ensured that production does not counteract the positive impact of this alternative fuel.
- Visit http://cfpub1.epa.gov/RBLC/ to learn more about the RACT/BACT/LAER Clearinghouse.